


Environmental Statement
EMAS STATEMENT REPORTING PLATFORM

Environmental Statement
EMAS EUROPEAN REGULATIONS

Environmental Statement
EMAS STATEMENT REPORTING PLATFORM
GRUPO CEMENTOS PORTLAND VALDERRIVAS:
MATAPORQUERA FACTORY
Annex IV.B Environmental statement
- A summary of the organisation's activities, products and services, the organisation's relationship to central organisations, if applicable, and a clear and unambiguous description of the scope of the EMAS registration, including a list of the sites included in this registration;
 |
General data |
Introductory Presentation
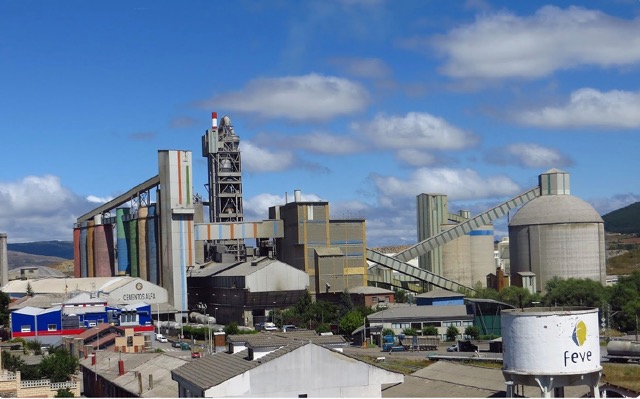
We present in this link our seventeenth Environmental Statement of the Mataporquera Factory of Cementos Alfa, S.A., belonging to the Grupo Cementos Portland Valderrivas, within the EMAS Regulation and the first one we publish in its 100% online and digital version. The objective is to provide our stakeholders with all the necessary information about those aspects and activities relevant to the environment associated with their activities in the exploitation of the marl and limestone quarry and the production of clinker, cement and mortar.
The Grupo Cementos Portland Valderrivas operates in the cement business based on a commitment to Sustainable Development, with an Environmental and Energy Management System (based on ISO 14001:2015 and ISO 50001:2018 standards) that takes into account the context of the factory with thinking based on risk and opportunity management, applying a life cycle approach life cycle approach of the manufactured products that contemplates:
- Planning of actions to control risks associated with environmental aspects and context analysis.
- Compliance with applicable requirements and performance evaluation
- Environmental improvement plans
- Action planning for the control of stakeholders' needs and expectations.
This Statement provides an update on the performance results for quantitative indicators related to environmental management aspects achieved in 2025: consumption of raw materials, fuels, electricity, and water; waste Recovery management; emissions to air, soil, and water; biodiversity initiatives; and environmental emergencies.
Indicators and results are prioritized, summarizing the environmental evolution with respect to previous Declarations to show improvements. All the contents of the Environmental Statement have been reviewed by the Management, with independent validation by AENOR CONFIA (the certificate can be seen at the end of the document).
 |
2025 |
 Centre/s
2
 Workers
109
 Surface
917.200 m2
 Activity in
Tn Cement + Mortar
645.674
Unit Ref.: Crushed Stone Production / Clinker Production / Cement Production / Mortar Production / Product Manufactured
Our organisation presents this validated Environmental Statement as part of our commitment to transparency and environmental improvement of our activities, operations and facilities.
LOCATION- MAIN CENTER
|
Description of the activity |
Activities and scope of the Environmental Statement
The company Cementos Alfa, S.A., with activities registered under NACE code 23.51, NACE 23.64 and NACE 08.11 for cement production, mortar manufacturing and stone quarrying, respectively, was founded in 1930. The company is part of the cement group Cementos Portland Valderrivas (GCPV), an industrial group present throughout the construction business cycle, made up of a large number of companies and present in Spain, with seven cement plants throughout the country, the United Kingdom and Tunisia, whose environmental organization is based on a hierarchical functional relationship between the Corporate Areas and the Operational and Business Responsibility Areas. The Mataporquera plant is located in the province of Cantabria and is dedicated to cement production using a dry-process kiln. The manufacturing facilities occupy an industrial area of 140,200m², distributed across three industrial parks measuring 88,000m², 41,200m², and 11,000m² , located in the municipality of Valdeolea, near the town center of the main settlement, Mataporquera, and are crossed by the Camesa River—a tributary of the Pisuerga River—and the RENFE railroad tracks. The marl and limestone quarry adjoins the plant and has an authorized area of 777,200square meters. Location of the plant and quarry: Bº La Estación s/n - 39410 Mataporquera (Cantabria)


Our organisation presents this validated Environmental Statement as part of our commitment to transparency and environmental improvement of our activities, operations and facilities.
|
Environmental management and governance approach |
Description of the Environmental Management System
The management system in place complies with the international standards UNE-EN-ISO 14001:2015—initially certified in 2003—and European Regulation 1221/2009 (EMAS III), which has been adapted to Regulation 1505/2017 and Regulation 2026/2018 —registered in 2008 under code ES-CA-000028—and is integrated as part of the Organization’s system, which adopts the principles of environmental management as a fundamental pillar of its operations. This management system, along with the audits and reviews conducted by management, enables the Organization to maintain a dynamic approach to environmental management, always guided by the following basic principles: Inspired by the philosophy of continuous improvement, it will be subject to the P-E-V-0 cycle (Plan - Execute - Verify - Optimize), and is supported by documents such as the Manual and General Procedures that respond to its interaction with the Corporate Departments and common between factories; as well as specific ones that reflect the particular operations and adapted to the legal requirements of each facility. The organizational context of the Mataporquera plant is determined by internal and external issues that influence the ability to achieve the objectives of the Environmental Management System. The external issues are mainly grouped into: needs and expectations of external stakeholders, geographical location, business situation, economic situation, legal and other applicable requirements and others. While internal issues include, in addition to internal stakeholders, aspects of the business group, environmental aspects, the production process itself, technological changes, management practices and others. The analysis of risks and opportunities is performed using qualitative or quantitative criteria. In the case of risks associated with environmental aspects and legal requirements, quantitative criteria are preferably used, as far as possible. The identification of risks and opportunities is carried out after the evaluation of environmental aspects, verification of applicable legal requirements and definition of the context and expectations and needs of interested parties. When qualitative criteria are used, we try to ensure that they are consistent and homogeneous based on experience and knowledge of the particular context of each plant. Thanks to the combination of probability and severity of the impact, their prioritization and the type of preventive action to be taken are established. The context analysis identifies risks and opportunities, and actions are studied and planned. Specifically, the main risks identified are: The main opportunities identified have been:
Organizational context
Determination of risks and opportunities
Risks
Opportunities
Location and contact
Address: Barrio de la Estación s/n, 39410 Mataporquera, Cantabria - Tel: 942.770.058 - Mail: jose.calvo@gcpv.com
Web: www.valderrivas.es
.
Main and secondary CNAE code: 23.51 Manufacture of cement, 23.64 Manufacture of mortar, 08.11 Quarrying of stone.
|
Environmental policy |
Organizational Policy
The Environmental and Energy Policy of Grupo Cementos Portland Valderrivas, approved in July 2022 by the Director of Operations for Spain and revised in May 2025, is aligned with the UNE-EN ISO 14001:2015 and UNE-EN ISO 50001:2018 standards. It reflects the commitment to environmental protection and pollution prevention, taking into account the context of its activities. Its principles include: providing resources to meet environmental objectives and regulations, exceeding legal minimums; promoting continuous improvement in facilities and environmental aspects with a life-cycle approach; establishing plans with resources for energy transition and decarbonization, aligned with sectoral, national, and international strategies; and integrating environmental and energy criteria into strategic planning, investments, and equipment procurement. Business success is linked to these sustainable practices.
- Resourcing
- Continuous improvement
- Energy transition and decarbonization
- Inclusion of environmental and energy considerations in strategic planning.
- Employee training and awareness
- Communication and outreach with stakeholders
- Energy efficiency
- Risk and opportunity management
- Fight against climate change
- Circular economy
- Water management
- Waste minimization
- Conservation of the environment
POLICY: Environmental and Energy Policy May 2025-dc7a5056
Mission
To develop, produce and market cement and construction materials, contributing to sustainable development, with special attention to safety and the environment, satisfying our shareholders, staff, customers and suppliers.
.
Vision
 |
Communication and participation |
Communication and stakeholder engagement
As in any business project, in the Mataporquera factory the participation of stakeholders in the development of the business is an essential element of its Strategy. Thus, we try to disclose our activities in a clear and transparent way in order to be more and better known. All communication activities have been influenced by the effect of the global pandemic.
Internal communication
Environmental Representatives are informed of the progress of the campaigns under the Environmental Monitoring Plan and of any environmental incidents. When preparing the environmental statement, the views of employee representatives are taken into account through meetings of the Environmental Committee and through communication initiatives.
In 2025, the monthly reporting system on environmental management at the plant continues, covering the results of measurement campaigns, waste management, Recovery relevant environmental aspects. This year, energy performance data has been included. Actions related to the Mataporquera plant are published in the magazine Portland Contigo.
Shareholders
The channels that ensure communication and dialogue between the Group and its shareholders are as follows:
- The General Shareholders' Meeting
- Specific call center service
- Specific e-mail: accionistas@valderrivas.es
- The corporate website in its section aimed exclusively at shareholders
Employees
The satisfaction and motivation of the Group's human team is one of our greatest challenges. We have developed different internal communication channels that provide our employees with continuous information on our activities while encouraging their participation and involvement in decision-making related to environmental issues:
- Environment and Energy Committee and Health and Safety Committee: These committees hold regular meetings to discuss day-to-day environmental issues, with a focus on Recovery . Participants include plant management, department heads, environmental representatives, and members of the works council.
- Environmental communiqués: provide employees with direct communication with the environmental department regarding environmental incidents or suggestions for improving aspects of the facilities.
- Awareness-raising sessions and Environment and Energy Committees: periodic meetings between Management and Department Heads and between Department Heads and their operators, and meetings with industrial management to discuss common issues of the group and establish strategies for action.
- Training sessions: established in accordance with the Annual Training Plan, this is a bidirectional tool through which aspects related to the Environment and Occupational Risk Prevention are transmitted. We have also attended more specific conferences and forums on environmental issues of interest.
- Internet portal: in accordance with current legislation, the Group makes its corporate website, www.valderrivas.es, available to the public, enabling it to comply with the requirements of the Transparency Law and the disclosure of environmental information.
The dissemination of relevant information on environmental matters, arising from environmental committees or promoted by the Company and employees, is done through personalized letters and the bulletin board.
External communication
Suppliers, auxiliary industry and customers
It is our goal to further our commitment to extending our Environmental Policy to suppliers and contractors, involving them in our environmental practices so that we can all work in an environmentally responsible manner. To this end, we provide them with guidelines for action and request information from our suppliers regarding their management practices, recognizing that the ultimate satisfaction of our customers’ needs depends on the quality of the entire supply chain.
At the company, our efforts are focused on offering competitive, high-quality products through our Quality Management System in accordance with UNE-EN-ISO 9001:2015, which ensures consistency in our primary commitment to our customers, carried out within a framework of respect for the environment. The communication channels established to meet the environmental information needs of these stakeholders are the Commercial Support Department and our Group’s website.
Public and private administrations
The Mataporquera factory collaborates with public and private institutions in the promotion of initiatives or projects of interest to the community through sponsorships, collaboration agreements, participation in conferences and other events, if circumstances permit.
National, regional and local administration
Cementos Alfa, S.A. collaborates with national and regional government agencies whenever requested to do so. In 2025, the company welcomed the Regional Minister and Director General of the Cantabria Government’s Department of Industry to its factory and delivered a presentation at the launch of the Cantabria Government’s Bioeconomy and Circular Economy Strategy, held at the Chamber of Commerce.
We hold regular meetings with the Mataporquera City Council, both formally and informally, to outline the company’s environmental initiatives, presenting, among other things, the results of our actions and our proposals for improvement. As has been the case for years, we have collaborated on the management of the festival program and the publication of the Valdeolea magazine.
Associations and business groups
From our factory, we collaborate with other business associations and groups within Cantabria, Spain, and Europe, either through the group to which we belong or through our direct participation as a member.
In this regard, our achievements have been shared for application by other companies in the sector through our membership in OFICEMEN, the Spanish Association of Cement Manufacturers; IECA (Spanish Institute of Cement and its Applications); and CEMBUREAU, the European Cement Manufacturers’ Association. We are an active member of the CEOE-CEPYME Environment Forum of Cantabria.
We participated in the CEOE-CEPYME of Cantabria’s “Industry as the Foundation of Sustainable Development” program with a presentation about the factory at the secondary school in Torrelavegas. This program involves introducing companies from Cantabria to educational institutions in order to raise awareness of the region’s industrial landscape.
Occasional participation in training sessions for the regional press and regional associations and administrations:
- Delivery of a lecture in the Circular Economy course as part of the University of Cantabria’s Senior Program and Micro-Credential in Decarbonization, Circular Economy, and Hydrogen.
- Participation in the Diario Montañés Innovation and Digitalization Forum.
- Visit by students from the University of Cantabria
- Presentation at the CCU CONECT conference on CO2 capture techniques.
Society in general
An essential element of our cultural tradition is the rootedness of our company in the territories in which we operate. For this reason, we have developed a broader vision in our relationship with social agents and stakeholders in the communities, improving the channels of communication, dialogue and collaboration.
Sustainability Reports
In accordance with the Grupo Cementos Portland Valderrivas 's Sustainability Reporting Guidelines, which constitute a balanced and reasonable presentation of the company's economic, environmental and social performance. In addition, we ae also actively participate in different social sponsorships, as well as donations of cement and mortar to local entities.
Environmental emergencies
Real environmental emergency situations and environmental drills allow us to evaluate and update the application of the Emergency Plans designed for the plant by the Occupational Risk Prevention Department and the environmental accident management procedures defined within the Environmental Management System.
The plant has a self-protection plan, updated in November 2022, that incorporates all environmental response measures in the event of an environmental emergency, in accordance with Royal Decree 840/2015 of September 21, which approves measures to control the risks inherent in major accidents involving hazardous substances.
In 2025, a fire broke out at the facility for the storage and dosing of solid alternative fuels for the main burner.
The incident was initially brought under control using internal resources and with the assistance of the Reinosa Fire Department. An analysis of the causes has led to a series of improvements aimed at enhancing fire prevention and suppression, to be implemented between 2025 and 2026.
Dangerous goods are unloaded in accordance with the International Agreement concerning the Carriage of Dangerous Goods by Road - ADR. We have a Safety Advisor.
Social information
Link here to our main social networks.
 |
 |
 |
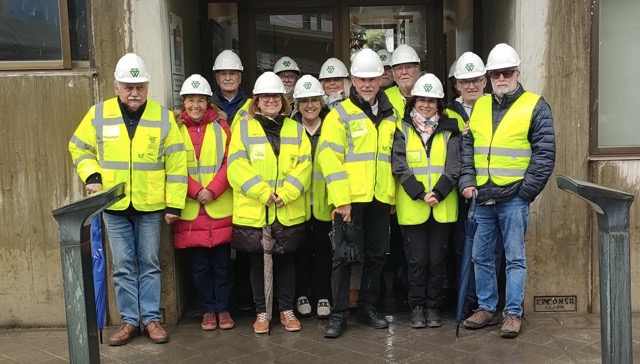
Visit by the Senior Group from the University of Cantabria.
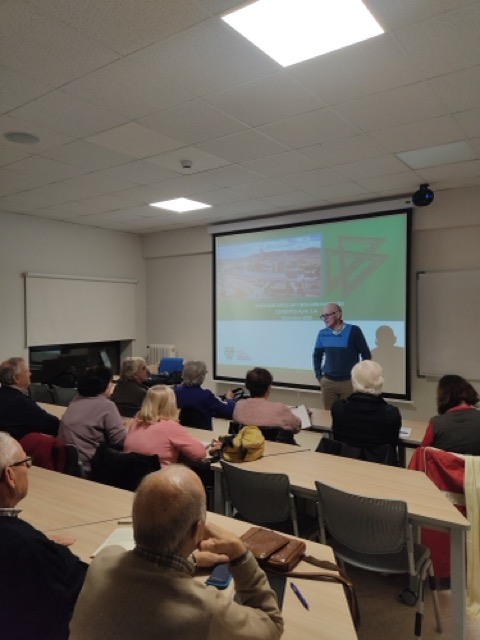
Presentation at the Senior Classroom, University of Cantabria.
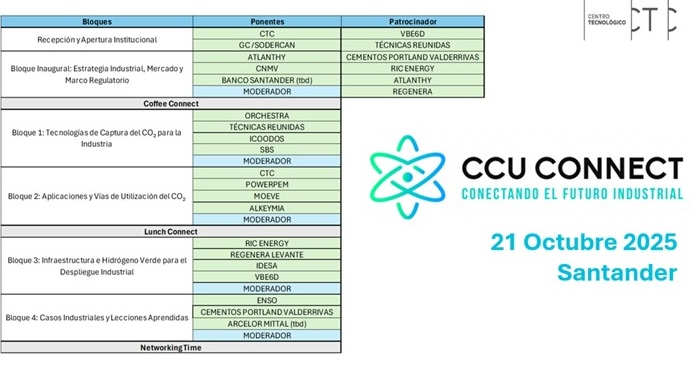
CO2 capture project.
 |
Environmental assessment and performance |
|
Key metrics |
◉ Global indicators 2025
Includes the sum of all the organisation's sites under the EMAS Register.
ENERGY CONSUMPTION

483,346.13MWh
• Renewable energy consumption: 69%
• Renewable energy generation:0%
WATER CONSUMPTION

145,114m³
• Supply network9.846%
Source: Network
TOTAL DISCHARGES

41,164m³
•100% public waterway
CO2 EMISSIONS

313,978 (ETS) *metric tons
• Indirect: 4.5%
• Direct 95.5%
WASTE

1,497.808tons
• Hazardous 1.127%
• Recovery 96.93%
* ETS-verified CO2 emissions are included. The percentage of direct data corresponds to Scope 1, and the percentage of indirect data corresponds to Scope 2.
Unit values on production/performance
0.749 MWh/Tons of Cement + Mortar
0.225 m³/Tons of Cement + Mortar
0.064 m³/Tons of Cement + Mortar
0.486 Tn/Tn Cement + Mortar
0.0023 Tn/Tn Cement + Mortar
Unit Ref: Tn Cement + Mortar Crushed Stone Production / Clinker Production / Cement Production / Mortar Production / Product Manufactured
|
Dimension of the activity |
Description of the main activity
The production process begins with the reception of limestone raw materials from the quarry, located next to the factory, in the municipality of Valdeolea, with an approximate surface area of 917,200 m2. The most relevant environmental impacts associated with quarrying are: visual impact, change in the morphology of the terrain, occupation of natural spaces, depletion of natural resources and impacts associated with quarrying, such as vibrations, noise and particle emissions, mainly. These previously homogenized limestones and marls, together with other raw materials of the same nature, give rise to raw meal, after a process of grinding and appropriate mixing. This raw meal, heated to over 1,450ºC using petroleum coke, previously ground, and other alternative fuels (tires, wood, meat meal, rubber, plastic and cocoa husks) in a horizontal rotary kiln and a cyclone tower, gives rise to the intermediate product, clinker, consisting mainly of calcium silicates, which are responsible for the irreversible hardening of cement in contact with water and/or air. The most relevant environmental impacts associated with the manufacture of cement and mortar are: atmospheric pollution from the grinding and combustion processes, global warming, noise emissions and the depletion of natural resources such as fossil fuels and energy. Its grinding, together with other additions and a setting regulator such as gypsum, in appropriate proportions, gives rise to cement, with specific chemical, physical and mechanical properties that are standardized according to the type of addition, from limestone to fly ash from coal-fired power plants or blast furnace slag, among others, and the fineness of the grinding. The final product, cement or mortar resulting from the mixture of cement and aggregates, is stored in silos for sale in bulk or subsequent bagging.

Evolution of production activity
Business performance
Activity by type
Type of productive activity
| HOLDING | COMPANY | SITE | STATUS | wdt_ID | userid | YEAR | rp | SCOPE | CENTER | MAGNITUDE | UNIT | ACTIVITY | %RECYCLED | % Hazardous | SALES (€) | DESTINATION COUNTRY | REF. REPORT | REMARKS | link route | post_author | post_type |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| GCPV | CEMENTOS ALFA, SA | PIG KILLER | VALIDATED | 274 | 2.089 | 2023 | PRODUCTION | Factory | 367.612,00 | t | Production of GREY CLINKER | Spain | EMAS | 2.089 | emas_statement | ||||||
| GCPV | CEMENTOS ALFA, SA | PIG KILLER | VALIDATED | 275 | 2.089 | 2024 | PRODUCTION | Factory | 398.372,00 | t | Production of GREY CLINKER | Spain | EMAS | 2.089 | emas_statement | ||||||
| GCPV | CEMENTOS ALFA, SA | PIG KILLER | VALIDATED | 278 | 2.089 | 2023 | PRODUCTION | Factory | 574.552,00 | t | Production of GREY CEMENT | Spain | EMAS | 2.089 | emas_statement | ||||||
| GCPV | CEMENTOS ALFA, SA | PIG KILLER | VALIDATED | 279 | 2.089 | 2024 | PRODUCTION | Factory | 582.772,00 | t | Production of GREY CEMENT | Spain | EMAS | 2.089 | emas_statement | ||||||
| GCPV | CEMENTOS ALFA, SA | PIG KILLER | VALIDATED | 282 | 2.089 | 2023 | PRODUCTION | Factory | 53.608,00 | t | Mortar production | Spain | EMAS | 2.089 | emas_statement | ||||||
| GCPV | CEMENTOS ALFA, SA | PIG KILLER | VALIDATED | 283 | 2.089 | 2024 | PRODUCTION | Factory | 58.090,00 | t | Mortar production | Spain | EMAS | 2.089 | emas_statement | ||||||
| GCPV | CEMENTOS ALFA, SA | PIG KILLER | VALIDATED | 286 | 2.089 | 2023 | PRODUCTION | Quarry | 579.797,00 | t | Extraction and production of CRUSHED STONE | Spain | EMAS | 2.089 | emas_statement | ||||||
| GCPV | CEMENTOS ALFA, SA | PIG KILLER | VALIDATED | 287 | 2.089 | 2024 | PRODUCTION | Quarry | 708.600,00 | t | Extraction and production of CRUSHED STONE | Spain | EMAS | 2.089 | emas_statement | ||||||
| GCPV | CEMENTOS ALFA, SA | PIG KILLER | VALIDATED | 472 | 2.089 | 2025 | PRODUCTION | Factory | 433.549,00 | t | Production of GREY CLINKER | Spain | EMAS | 2.089 | emas_statement | ||||||
| GCPV | CEMENTOS ALFA, SA | PIG KILLER | VALIDATED | 473 | 2.089 | 2025 | PRODUCTION | Factory | 581.843,00 | t | Production of GREY CEMENT | Spain | EMAS | 2.089 | emas_statement | ||||||
| GCPV | CEMENTOS ALFA, SA | PIG KILLER | VALIDATED | 474 | 2.089 | 2025 | PRODUCTION | Factory | 63.831,00 | t | Mortar production | Spain | EMAS | 2.089 | emas_statement | ||||||
| GCPV | CEMENTOS ALFA, SA | PIG KILLER | VALIDATED | 475 | 2.089 | 2025 | PRODUCTION | Quarry | 663.668,00 | t | Extraction and production of CRUSHED STONE | Spain | EMAS | 2.089 | emas_statement | ||||||
Evolution of production activity
In 2025, clinker production continued to rise, leading to an increase in the extraction of stone from the quarry needed for its manufacture. Sales of cement and mortar also continued to rise.
The wide range of products manufactured allows for the ideal selection based on the application. The cements marketed in 2025 from the Mataporquera plant come in six different grades, all certified with the AENOR N Product Certification mark as well as CE marking, complying with current legislation and the requirements of standards UNE-EN 197-1 and UNE-80.303-1. The production percentages for each type of cement in 2025 were as follows:
CEM I 52.5 R ( UNE-EN 197-1 for the domestic and export markets) 0.69%
CEM III/B 32.5 N/SR ( UNE 80.303-1 for the domestic market) 1.34%
CEM II/BL 32.5 N ( UNE-EN 197-1 for the domestic market) 1.04%
CEM II/A-L 42.5 R ( UNE-EN 197-1 for the domestic market) 42.40%
CEM I/52.5 N ma* (UNE-EN 197-1 for Domestic and Export Markets) 53.56%
CEM IV/A(V) 42.5 N-SR ( UNE 80.303-1 for the domestic market) 0.96%
Our cements have a Safety Data Sheet that allows customers a safe and responsible use of the product, due to its irritant character associated to its alkalinity, mainly.
*ma: cement with moderate alkali content

 |
Energy use and management |
Energy management
The transformations associated with the manufacture of clinker and cement, which include processes of grinding, mixing, firing and milling of raw materials, fuels and clinker, involve high energy consumption. This energy comes mainly from fuels - thermal energy - and electricity - electrical energy -. That is why our organization integrates to its Environmental Management System new energy efficiency control and auditing procedures under the UNE EN ISO 50001:2018 standard. The fossil fuels commonly used in the manufacture of clinker are those derived from petroleum, such as coal, petroleum coke and fuel oil. Oil gas is also used in vehicles, generators and heating boilers. Electric power is used in the process for grinding, storage and metering of the raw material, fuels and final product. For several years now, the strategic policy of Grupo Cementos Portland Valderrivas on harnessing the energy contained in waste, partially replacing fossil fuels with alternative fuels—some of which have a high biomass content and are carbon-neutral in terms of emissions that contribute to global warming. Thus, at the Mataporquera plant, shredded tires (NFU), animal meal, olive pomace, solid waste-derived fuels (plastics, rubber, wood, paper, etc.), and fuel blending (mixtures of Hazardous liquid alternative fuels: a mixture of paints and solvents) have been used to replace petroleum coke and coal. The consumption tables contemplate the following energy uses:
Environmental management and control
Fuel consumption
The percentage of thermal energy replaced by waste-derived fuels with calorific value in 2025 has decreased compared to previous years, reaching 60.1% compared to 64.3% in 2024 and 64% in 2023. This decline was due to a drop in consumption caused by a fire at the storage and metering facility for solid alternative fuels used by the main burner.
Environmental improvement targets are set to achieve a 70% thermal contribution from alternative fuels. Modifications to the tower kiln facility are being studied, and work continues on optimizing the expert control system for the tower kiln calcination line to improve energy efficiency and increase the Recovery alternative fuels.
Electricity consumption
Specific electricity consumption has increased from 12.53 MWh per ton of cement in 2023 and 116.07 MWh per ton of cement in 2024 to 119 MWh per ton of cement in 2025. This consumption depends on the purchased clinker used in cement production.
The trend in relevant consumption by facility shows a decrease in Table 2024 vs. 2025
In 2025, improvements have been implemented at facilities to reduce electricity consumption in processes: replacement of balls in the cement mill, modification of the raw mill configuration, repair of refractory bricks in the kiln, implementation of the expert kiln control system, and replacement of compressor No. 1 in the tower, as well as replacement of electric motors with more efficient ones. These measures are being evaluated for eligibility for energy savings certificates (CAEs).
Evolution of specific metrics and ratios
Units of energy consumption in MWh and their ratios associated with the activity.
Energy consumption by fuel
Uses of energy
The energy magnitudes are always parameterized in MWh, showing in each cell its transformation to GJ, by means of the standard MWh*3.6 conversion (factor officially recognized and used by the SI (BIPM), Eurostat, IEA, IPCC and in Spain by MITECO).
| wdt_ID | userid | Year | Center | Units Pr. | Unit | Uses / Info | Electricity Consumption (MWh) | LNG/LPG consumption (MWh) | Oil / Coal (MWh) | Other Consumption (MWh) | gasnatural_gl | tankers_gl | other_gl | ind_gasnatural_gl | ind_petroliferos_gl | ind_other_gl | post_type | post_author | Electricity Ratio (Units Pr. | GN RatioPr.Units Pr. | Gasoline Ratio (Units Pr. | Ratio of other MWh toUnits Pr. | Total consumption ratio (Units Pr. | Total consumption (MWh) | Ratio of Total GJ/ Udp | Total GJ | Electrical in GJ | Electric GJ/udp Ratio |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| 188 | 2.089 | 2023 | Factory | 628.160,000 | t Product manufactured | Fuel for factory transportation | 0,000 | 0,000 | 844,166 | 0,000 | 0,000 | 3.038,998 | 0,000 | 0,000 | 0,005 | 0,000 | attachment | 2.089 | 0,000 | 0,000 | 0,001 | 0,000 | 0,001 | 844,166 | 0,005 | 3.038,998 | 0,000 | 0,000 |
| 189 | 2.089 | 2023 | Quarry | 579.797,000 | t Crushed stone | Fuel for quarry transportation | 0,000 | 0,000 | 1.308,888 | 0,000 | 0,000 | 4.711,997 | 0,000 | 0,000 | 0,008 | 0,000 | attachment | 2.089 | 0,000 | 0,000 | 0,002 | 0,000 | 0,002 | 1.308,888 | 0,008 | 4.711,997 | 0,000 | 0,000 |
| 190 | 2.089 | 2023 | Factory | 628.160,000 | t Product manufactured | TOTAL Electricity for Factory Production | 64.653,610 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | attachment | 2.089 | 0,103 | 0,000 | 0,000 | 0,000 | 0,103 | 64.653,610 | 0,371 | 232.752,996 | 232.752,996 | 0,371 |
| 191 | 2.089 | 2023 | Quarry | 628.160,000 | t Product manufactured | Electricity for Quarry Production | 1.322,009 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | attachment | 2.089 | 0,002 | 0,000 | 0,000 | 0,000 | 0,002 | 1.322,009 | 0,008 | 4.759,232 | 4.759,232 | 0,008 |
| 194 | 2.089 | 2024 | Factory | 640.862,000 | t Product manufactured | Fuel for factory transportation | 0,000 | 0,000 | 782,222 | 0,000 | 0,000 | 2.815,999 | 0,000 | 0,000 | 0,004 | 0,000 | attachment | 2.089 | 0,000 | 0,000 | 0,001 | 0,000 | 0,001 | 782,222 | 0,004 | 2.815,999 | 0,000 | 0,000 |
| 195 | 2.089 | 2024 | Quarry | 708.600,000 | t Crushed stone | Fuel for quarry transportation | 0,000 | 0,000 | 1.455,000 | 0,000 | 0,000 | 5.238,000 | 0,000 | 0,000 | 0,007 | 0,000 | attachment | 2.089 | 0,000 | 0,000 | 0,002 | 0,000 | 0,002 | 1.455,000 | 0,007 | 5.238,000 | 0,000 | 0,000 |
| 196 | 2.089 | 2024 | Factory | 640.862,000 | t Product manufactured | TOTAL Electricity for Factory Production | 67.640,740 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | attachment | 2.089 | 0,106 | 0,000 | 0,000 | 0,000 | 0,106 | 67.640,740 | 0,380 | 243.506,664 | 243.506,664 | 0,380 |
| 197 | 2.089 | 2024 | Quarry | 640.862,000 | t Product manufactured | Electricity for Quarry Production | 1.297,500 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | attachment | 2.089 | 0,002 | 0,000 | 0,000 | 0,000 | 0,002 | 1.297,500 | 0,007 | 4.671,000 | 4.671,000 | 0,007 |
| 252 | 2.089 | 2023 | Factory | 367.612,000 | t Clinker fabricated | Petroleum Coke and Coal Consumption | 0,000 | 0,000 | 133.088,913 | 0,000 | 0,000 | 479.120,087 | 0,000 | 0,000 | 1,303 | 0,000 | attachment | 2.089 | 0,000 | 0,000 | 0,362 | 0,000 | 0,362 | 133.088,913 | 1,303 | 479.120,087 | 0,000 | 0,000 |
| 253 | 2.089 | 2023 | Factory | 367.612,000 | t Clinker fabricated | Fuel oil consumption | 0,000 | 0,000 | 1.283,822 | 0,000 | 0,000 | 4.621,759 | 0,000 | 0,000 | 0,013 | 0,000 | attachment | 2.089 | 0,000 | 0,000 | 0,003 | 0,000 | 0,003 | 1.283,822 | 0,013 | 4.621,759 | 0,000 | 0,000 |
| 254 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | Petroleum Coke and Coal Consumption | 0,000 | 0,000 | 137.600,278 | 0,000 | 0,000 | 495.361,001 | 0,000 | 0,000 | 1,243 | 0,000 | attachment | 2.089 | 0,000 | 0,000 | 0,345 | 0,000 | 0,345 | 137.600,278 | 1,243 | 495.361,001 | 0,000 | 0,000 |
| 255 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | Fuel oil consumption | 0,000 | 0,000 | 1.354,522 | 0,000 | 0,000 | 4.876,279 | 0,000 | 0,000 | 0,012 | 0,000 | attachment | 2.089 | 0,000 | 0,000 | 0,003 | 0,000 | 0,003 | 1.354,522 | 0,012 | 4.876,279 | 0,000 | 0,000 |
| 257 | 2.089 | 2023 | Factory | 367.612,000 | t Clinker fabricated | Fuel blending consumption | 0,000 | 0,000 | 99.459,860 | 0,000 | 0,000 | 358.055,496 | 0,000 | 0,000 | 0,974 | 0,000 | attachment | 2.089 | 0,000 | 0,000 | 0,271 | 0,000 | 0,271 | 99.459,860 | 0,974 | 358.055,496 | 0,000 | 0,000 |
| 258 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | Fuel blending consumption | 0,000 | 0,000 | 102.248,231 | 0,000 | 0,000 | 368.093,632 | 0,000 | 0,000 | 0,924 | 0,000 | attachment | 2.089 | 0,000 | 0,000 | 0,257 | 0,000 | 0,257 | 102.248,231 | 0,924 | 368.093,632 | 0,000 | 0,000 |
| 260 | 2.089 | 2023 | Factory | 367.612,000 | t Clinker fabricated | Consumption of tires as fuel | 0,000 | 0,000 | 55.459,189 | 22.531,514 | 0,000 | 199.653,080 | 81.113,450 | 0,000 | 0,543 | 0,221 | attachment | 2.089 | 0,000 | 0,000 | 0,151 | 0,061 | 0,212 | 77.990,703 | 0,764 | 280.766,531 | 0,000 | 0,000 |
| 261 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | Consumption of tires as fuel | 0,000 | 0,000 | 59.922,759 | 24.344,937 | 0,000 | 215.721,932 | 87.641,773 | 0,000 | 0,542 | 0,220 | attachment | 2.089 | 0,000 | 0,000 | 0,150 | 0,061 | 0,212 | 84.267,696 | 0,762 | 303.363,706 | 0,000 | 0,000 |
| 263 | 2.089 | 2023 | Factory | 367.612,000 | t Clinker fabricated | Consumption of Orujillo as fuel | 0,000 | 0,000 | 0,000 | 2.358,146 | 0,000 | 0,000 | 8.489,326 | 0,000 | 0,000 | 0,023 | attachment | 2.089 | 0,000 | 0,000 | 0,000 | 0,006 | 0,006 | 2.358,146 | 0,023 | 8.489,326 | 0,000 | 0,000 |
| 264 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | Consumption of Orujillo as fuel | 0,000 | 0,000 | 0,000 | 4.853,274 | 0,000 | 0,000 | 17.471,786 | 0,000 | 0,000 | 0,044 | attachment | 2.089 | 0,000 | 0,000 | 0,000 | 0,012 | 0,012 | 4.853,274 | 0,044 | 17.471,786 | 0,000 | 0,000 |
| 266 | 2.089 | 2023 | Factory | 367.612,000 | t Clinker fabricated | Wood consumption as fuel | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | attachment | 2.089 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 |
| 267 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | Wood consumption as fuel | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | attachment | 2.089 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 |
| 269 | 2.089 | 2023 | Factory | 367.612,000 | t Clinker fabricated | Consumption of husk as fuel | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | attachment | 2.089 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 |
| 270 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | Consumption of husk as fuel | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | attachment | 2.089 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 |
| 272 | 2.089 | 2023 | Factory | 367.612,000 | t Clinker fabricated | Consumption of flour as fuel | 0,000 | 0,000 | 0,000 | 56.611,435 | 0,000 | 0,000 | 203.801,166 | 0,000 | 0,000 | 0,554 | attachment | 2.089 | 0,000 | 0,000 | 0,000 | 0,154 | 0,154 | 56.611,435 | 0,554 | 203.801,166 | 0,000 | 0,000 |
| 273 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | Consumption of flour as fuel | 0,000 | 0,000 | 0,000 | 48.927,043 | 0,000 | 0,000 | 176.137,355 | 0,000 | 0,000 | 0,442 | attachment | 2.089 | 0,000 | 0,000 | 0,000 | 0,123 | 0,123 | 48.927,043 | 0,442 | 176.137,355 | 0,000 | 0,000 |
| 275 | 2.089 | 2023 | Factory | 367.612,000 | t Clinker fabricated | Consumption of RDF as fuel | 0,000 | 0,000 | 221,495 | 1.975,876 | 0,000 | 797,382 | 7.113,154 | 0,000 | 0,002 | 0,019 | attachment | 2.089 | 0,000 | 0,000 | 0,001 | 0,005 | 0,006 | 2.197,371 | 0,022 | 7.910,536 | 0,000 | 0,000 |
| 276 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | Consumption of RDF as fuel | 0,000 | 0,000 | 1.124,590 | 8.357,621 | 0,000 | 4.048,524 | 30.087,436 | 0,000 | 0,010 | 0,076 | attachment | 2.089 | 0,000 | 0,000 | 0,003 | 0,021 | 0,024 | 9.482,211 | 0,086 | 34.135,960 | 0,000 | 0,000 |
| 278 | 2.089 | 2023 | Factory | 367.612,000 | t Clinker fabricated | Marro consumption as fuel | 0,000 | 0,000 | 0,000 | 22,500 | 0,000 | 0,000 | 81,000 | 0,000 | 0,000 | 0,000 | attachment | 2.089 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 22,500 | 0,000 | 81,000 | 0,000 | 0,000 |
| 279 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | Marro consumption as fuel | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | attachment | 2.089 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 |
| 390 | 2.089 | 2025 | Quarry | 663.668,000 | t Product manufactured | Electricity for Quarry Production | 1.355,907 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | attachment | 2.089 | 0,002 | 0,000 | 0,000 | 0,000 | 0,002 | 1.355,907 | 0,007 | 4.881,265 | 4.881,265 | 0,007 |
| 391 | 2.089 | 2025 | Factory | 645.674,000 | t Product manufactured | TOTAL Electricity for Factory Production | 68.102,621 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | attachment | 2.089 | 0,105 | 0,000 | 0,000 | 0,000 | 0,105 | 68.102,621 | 0,380 | 245.169,436 | 245.169,436 | 0,380 |
| 392 | 2.089 | 2025 | Factory | 645.674,000 | t Product manufactured | Fuel for factory transportation | 0,000 | 0,000 | 870,037 | 0,000 | 0,000 | 3.132,133 | 0,000 | 0,000 | 0,005 | 0,000 | attachment | 2.089 | 0,000 | 0,000 | 0,001 | 0,000 | 0,001 | 870,037 | 0,005 | 3.132,133 | 0,000 | 0,000 |
| 393 | 2.089 | 2025 | Quarry | 663.668,000 | t Crushed stone | Fuel for quarry transportation | 0,000 | 0,000 | 1.598,814 | 0,000 | 0,000 | 5.755,730 | 0,000 | 0,000 | 0,009 | 0,000 | attachment | 2.089 | 0,000 | 0,000 | 0,002 | 0,000 | 0,002 | 1.598,814 | 0,009 | 5.755,730 | 0,000 | 0,000 |
| 394 | 2.089 | 2025 | Factory | 433.549,000 | t Clinker fabricated | Petroleum Coke and Coal Consumption | 0,000 | 0,000 | 168.490,619 | 0,000 | 0,000 | 606.566,228 | 0,000 | 0,000 | 1,399 | 0,000 | attachment | 2.089 | 0,000 | 0,000 | 0,389 | 0,000 | 0,389 | 168.490,619 | 1,399 | 606.566,228 | 0,000 | 0,000 |
| 395 | 2.089 | 2025 | Factory | 433.549,000 | t Clinker fabricated | Fuel oil consumption | 0,000 | 0,000 | 1.142,422 | 0,000 | 0,000 | 4.112,719 | 0,000 | 0,000 | 0,009 | 0,000 | attachment | 2.089 | 0,000 | 0,000 | 0,003 | 0,000 | 0,003 | 1.142,422 | 0,009 | 4.112,719 | 0,000 | 0,000 |
| 396 | 2.089 | 2025 | Factory | 433.549,000 | t Clinker fabricated | Fuel blending consumption | 0,000 | 0,000 | 84.545,542 | 0,000 | 0,000 | 304.363,951 | 0,000 | 0,000 | 0,702 | 0,000 | attachment | 2.089 | 0,000 | 0,000 | 0,195 | 0,000 | 0,195 | 84.545,542 | 0,702 | 304.363,951 | 0,000 | 0,000 |
| 397 | 2.089 | 2025 | Factory | 433.549,000 | t Clinker fabricated | Consumption of tires as fuel | 0,000 | 0,000 | 51.609,549 | 20.967,513 | 0,000 | 185.794,376 | 75.483,047 | 0,000 | 0,429 | 0,174 | attachment | 2.089 | 0,000 | 0,000 | 0,119 | 0,048 | 0,167 | 72.577,062 | 0,603 | 261.277,423 | 0,000 | 0,000 |
| 398 | 2.089 | 2025 | Factory | 433.549,000 | t Clinker fabricated | Consumption of Orujillo as fuel | 0,000 | 0,000 | 0,000 | 12.234,222 | 0,000 | 0,000 | 44.043,199 | 0,000 | 0,000 | 0,102 | attachment | 2.089 | 0,000 | 0,000 | 0,000 | 0,028 | 0,028 | 12.234,222 | 0,102 | 44.043,199 | 0,000 | 0,000 |
| 399 | 2.089 | 2025 | Factory | 433.549,000 | t Clinker fabricated | Wood consumption as fuel | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | attachment | 2.089 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 |
| 400 | 2.089 | 2025 | Factory | 433.549,000 | t Clinker fabricated | Consumption of husk as fuel | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | attachment | 2.089 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 | 0,000 |
| 401 | 2.089 | 2025 | Factory | 433.549,000 | t Clinker fabricated | Consumption of flour as fuel | 0,000 | 0,000 | 0,000 | 56.234,207 | 0,000 | 0,000 | 202.443,145 | 0,000 | 0,000 | 0,467 | attachment | 2.089 | 0,000 | 0,000 | 0,000 | 0,130 | 0,130 | 56.234,207 | 0,467 | 202.443,145 | 0,000 | 0,000 |
| 402 | 2.089 | 2025 | Factory | 433.549,000 | t Clinker fabricated | Consumption of RDF as fuel | 0,000 | 0,000 | 3.275,450 | 15.388,080 | 0,000 | 11.791,620 | 55.397,088 | 0,000 | 0,027 | 0,128 | attachment | 2.089 | 0,000 | 0,000 | 0,008 | 0,035 | 0,043 | 18.663,530 | 0,155 | 67.188,708 | 0,000 | 0,000 |
| Year | Center | |||||||||||||||||||||||||||
| ∑ = 19,275,928.000 |
Note: Recovery cement plants is considered one of the most efficient methods for the complete destruction of organic compounds, while inorganic compounds are incorporated into the raw materials and leave the process as part of the clinker. It also reduces overall greenhouse gas emissions, contributes to sustainable development by conserving non-renewable energy resources, prevents the accumulation of waste in landfills by managing it in a safe and environmentally friendly manner, reduces cement manufacturing costs, and maintains environmental safety (www.recuperaresiduosencementeras.org).
|
Renewable energies |
Energías Renovables
Configuración Colores
| wdt_ID | userid | Year | Center | Units Pr. | Units | Uses | Renewable consumed from third parties (MWh) | Renewable consumed self-generated (MWh) | Renewable generated (MWh) | post_author | Total renewable energy consumed (MWh) | Ratio of MWh of renewable energy consumed toUnits Pr. | Ratio of MWh of renewable energy generated perUnits of Pr. |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| 85 | 2.089 | 2023 | Factory + Quarry | 628.160,000 | t Product manufactured | Various uses | 45.461,440 | 2.089 | 45.461,440 | 0,0724 | 0,0000 | ||
| 87 | 2.089 | 2023 | Factory | 367.612,000 | t Clinker fabricated | Various uses | 83.554,856 | 2.089 | 83.554,856 | 0,2273 | 0,0000 | ||
| 89 | 2.089 | 2024 | Factory + Quarry | 640.862,000 | t Product manufactured | Various uses | 52.510,250 | 2.089 | 52.510,250 | 0,0819 | 0,0000 | ||
| 90 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | Various uses | 85.910,049 | 2.089 | 85.910,049 | 0,2157 | 0,0000 | ||
| 181 | 2.089 | 2025 | Factory + Quarry | 645.674,000 | t Product manufactured | Various uses | 45.579,290 | 2.089 | 45.579,290 | 0,0706 | 0,0000 | ||
| 182 | 2.089 | 2025 | Factory | 433.549,000 | t Clinker fabricated | Various uses | 105.127,451 | 2.089 | 105.127,451 | 0,2425 | 0,0000 | ||
| wdt_ID | userid | Year | Center | Units | post_author | ||||||||
| ∑ = 3,114,229.000 |
Note: Renewable energy is the sum of the substitution of biomass in kiln fuel and the MWh of renewable energy in the electricity mix. The use of biomass in clinker production was 25.4% in 2025, compared to 22.4% in 2023 and 22.1% in 2024. Biomass is a fuel with low calorific value, so its use requires a blend with other types of fuels with high calorific value, typically fossil fuels such as petroleum coke, fuel blending, tires, or coal. The improvement target for 2030 is set at achieving 35% biomass use. The percentage of renewable energy in the electricity generation mix is due to the signing of long-term supply contracts with photovoltaic plant operators. Additionally, the Mataporquera plant has signed an agreement with the company managing the wind farms currently under development at the Mataporquera hub to feed 100% of the renewable energy generated into the grid via its electrical substation. In 2025, 69% of the electricity mix came from renewable sources.
 |
Water use and management |
Water management
The sources of water supply used in our center are, on the one hand, the catchment of the Camesa river for cooling facilities and equipment, the public supply of the City of Valdeolea that supplies water for drinking use and, finally, the use of water from the quarry pond under authorization since 2023.
Environmental management and control
Between 2022 and 2025, there was a gradual increase in water consumption due to the need to irrigate the quarry to reduce dust emissions, primarily during the summer months. In 2025, there was also additional water consumption due to firefighting efforts at the storage and metering facilities for the main burner of solid alternative fuels.
Some of the significant environmental issues and risks identified in this Statement include complaints from residents of Mataporquera regarding dust pollution, with the quarry being one of the main sources of this problem during the summer. The way to reduce emissions is by watering the vehicle access roads and the material piled up at the quarry faces prior to the crushing process, which involves water consumption that depends on dust emissions and wind direction.
Evolution of specific metrics and ratios
Water consumption (m³) and ratios
Water Uses
| state | wdt_ID | userid | Year | Center | Units Pr. | Unit | Origin of water | Uses | m3 | ID | post_author | Ratio (Units Pr. |
|---|---|---|---|---|---|---|---|---|---|---|---|---|
| VALIDATED | 177 | 2.089 | 2023 | Factory | 628.160,000 | t Product manufactured | Surface catchment | Production | 67.833,000 | 138.963 | 2.089 | 0,107987 |
| VALIDATED | 178 | 2.089 | 2023 | Factory | 628.160,000 | t Product manufactured | Public supply network | Production | 13.270,000 | 138.963 | 2.089 | 0,021125 |
| VALIDATED | 180 | 2.089 | 2023 | Quarry | 579.797,000 | t Crushed stone | Public supply network | Production | 77,000 | 138.963 | 2.089 | 0,000133 |
| VALIDATED | 181 | 2.089 | 2024 | Factory | 640.862,000 | t Product manufactured | Surface catchment | Production | 97.459,000 | 138.963 | 2.089 | 0,152075 |
| VALIDATED | 182 | 2.089 | 2024 | Factory | 640.862,000 | t Product manufactured | Public supply network | Production | 16.578,000 | 138.963 | 2.089 | 0,025868 |
| VALIDATED | 183 | 2.089 | 2024 | Quarry | 708.600,000 | t Crushed stone | Public supply network | Production | 139,000 | 138.963 | 2.089 | 0,000196 |
| VALIDATED | 184 | 2.089 | 2023 | Quarry | 579.797,000 | t Crushed stone | Surface catchment | Various uses | 2.014,000 | 138.963 | 2.089 | 0,003474 |
| VALIDATED | 185 | 2.089 | 2024 | Quarry | 708.600,000 | t Crushed stone | Surface catchment | Various uses | 2.060,000 | 138.963 | 2.089 | 0,002907 |
| VALIDATED | 359 | 2.089 | 2025 | Factory | 645.674,000 | t Product manufactured | Surface catchment | Production | 128.831,000 | 138.963 | 2.089 | 0,199529 |
| VALIDATED | 360 | 2.089 | 2025 | Factory | 645.674,000 | t Product manufactured | Public supply network | Production | 14.213,000 | 138.963 | 2.089 | 0,022013 |
| VALIDATED | 361 | 2.089 | 2025 | Quarry | 663.668,000 | t Crushed stone | Public supply network | Production | 75,000 | 138.963 | 2.089 | 0,000113 |
| VALIDATED | 362 | 2.089 | 2025 | Quarry | 663.668,000 | t Crushed stone | Surface catchment | Various uses | 1.957,000 | 138.963 | 2.089 | 0,002949 |
| VALIDATED | 363 | 2.089 | 2025 | Factory | 645.674,000 | t Product manufactured | Surface catchment | Production | 38,000 | 138.963 | 2.089 | 0,000059 |
| state | wdt_ID | userid | Year | Center | Unit | Origin of water | Uses | ID | post_author |
Note:
 |
Waste water discharge management |
Wastewater management
Our center channels the discharge of water into the Camesa River, carrying out controls every four months at all authorized discharge points to check that their characteristics are adequate to the discharge regulations and in order to preserve the quality of the receiving environment. The sanitary water from the factory is treated in our wastewater treatment plants with physical and chemical treatment. The sanitary water from the quarry passes through a water treatment plant before infiltration into the ground. Rainwater from the factory undergoes a process of settling and separation of oils and fats. Water from the cooling system can be discharged, although the closed-loop system prevents this discharge, which would only occur in emergency situations. Rainwater from the quarry is directed to the settling pond before being discharged into the Camesa River. Compliance with the limit values established in the Environmental Authorization of the Mataporquera factory has been guaranteed, and no exceedance of these values has been recorded. The discharge limits have also been complied with in the inspections carried out by technicians from the Duero Hydrographic Confederation to verify the quality of the water discharged. The maximum value of the four campaigns carried out for each pollutant and discharge point is presented due to its significance as it is the closest to the discharge limit value.
Environmental management and control
Public watercourse receiving the discharge: Camesa River
Evolution of specific metrics and ratios
| state | wdt_ID | userid | Year | Center | Units Pr. | Unit | Total Volume m3 | Ratio (Units Pr. | Destination | Pollutant | Concentration | Limit | Conc. unit | Mass value kg | RatioPr.Units Pr. | ID | post_author |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| VALIDATED | 580 | 2.089 | 2023 | Factory / CHECK POINT 1 PLUVIAL WATERS | 628.160,000 | t Product manufactured | 0,000 | Public waterway | pH | 8,170 | 5,5-9,5 | pH | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 581 | 2.089 | 2023 | Factory / CHECK POINT 1 PLUVIAL WATERS | 628.160,000 | t Product manufactured | 0,000 | Public waterway | Conductivity | 243,000 | 1.000 | ( μS/cm ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 582 | 2.089 | 2023 | Factory / CHECK POINT 1 PLUVIAL WATERS | 628.160,000 | t Product manufactured | 0,000 | Public waterway | Suspended matter | 16,000 | 50 | ( mg/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 583 | 2.089 | 2023 | Factory / CHECK POINT 1 PLUVIAL WATERS | 628.160,000 | t Product manufactured | 0,000 | Public waterway | COD | 32,000 | 100 | ( mgO2/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 584 | 2.089 | 2023 | Factory / CHECK POINT 1 PLUVIAL WATERS | 628.160,000 | t Product manufactured | 0,000 | Public waterway | Oils and fats | 0,500 | 10 | ( mg/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 585 | 2.089 | 2023 | Factory / CONTROL POINT 2 SANITARY WATERS | 628.160,000 | t Product manufactured | 0,000 | Public waterway | pH | 8,400 | 5,5-9,5 | pH | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 586 | 2.089 | 2023 | Factory / CONTROL POINT 2 SANITARY WATERS | 628.160,000 | t Product manufactured | 0,000 | Public waterway | Suspended matter | 19,000 | 60 | ( mg/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 587 | 2.089 | 2023 | Factory / CONTROL POINT 2 SANITARY WATERS | 628.160,000 | t Product manufactured | 0,000 | Public waterway | COD | 68,000 | 150 | ( mgO2/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 588 | 2.089 | 2023 | Factory / CONTROL POINT 2 SANITARY WATERS | 628.160,000 | t Product manufactured | 0,000 | Public waterway | DBO 5 | 30,000 | 90 | ( mgO2/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 589 | 2.089 | 2023 | Factory / CONTROL POINT 4 PLUVIAL WATERS | 628.160,000 | t Product manufactured | 0,000 | Public waterway | pH | 8,500 | 5,5-9,5 | pH | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 590 | 2.089 | 2023 | Factory / CONTROL POINT 4 PLUVIAL WATERS | 628.160,000 | t Product manufactured | 0,000 | Public waterway | Suspended matter | 14,000 | 50 | ( mg/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 591 | 2.089 | 2023 | Factory / CONTROL POINT 4 PLUVIAL WATERS | 688.431,000 | t Product manufactured | 0,000 | Public waterway | COD | 23,000 | 100 | ( mgO2/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 592 | 2.089 | 2023 | Factory / CONTROL POINT 4 PLUVIAL WATERS | 628.160,000 | t Product manufactured | 0,000 | Public waterway | Oils and fats | 5,600 | 10 | ( mg/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 593 | 2.089 | 2023 | Factory / CONTROL POINT 4 PLUVIAL WATERS | 628.160,000 | t Product manufactured | 0,000 | Public waterway | Hydrocarbons | 3,200 | 5 | ( mg/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 594 | 2.089 | 2023 | Factory / CHECK POINT 5 SANITARY WATERS | 628.160,000 | t Product manufactured | 0,000 | Public waterway | pH | 8,400 | 5,5-9,5 | pH | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 595 | 2.089 | 2023 | Factory / CHECK POINT 5 SANITARY WATERS | 628.160,000 | t Product manufactured | 0,000 | Public waterway | Suspended matter | 41,000 | 60 | ( mg/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 596 | 2.089 | 2023 | Factory / CHECK POINT 5 SANITARY WATERS | 628.160,000 | t Product manufactured | 0,000 | Public waterway | COD | 124,000 | 150 | ( mgO2/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 597 | 2.089 | 2023 | Factory / CHECK POINT 5 SANITARY WATERS | 628.160,000 | t Product manufactured | 0,000 | Public waterway | DBO 5 | 60,000 | 90 | ( mgO2/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 598 | 2.089 | 2023 | Quarry / SANITARY WATER CONTROL POINT IN QUARRY | 579.797,000 | t Crushed stone | 0,000 | Public waterway | pH | 8,710 | 6-9 | pH | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 599 | 2.089 | 2023 | Quarry / SANITARY WATER CONTROL POINT IN QUARRY | 579.797,000 | t Crushed stone | 0,000 | Public waterway | Suspended matter | 9,000 | 90 | ( mg/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 600 | 2.089 | 2023 | Quarry / SANITARY WATER CONTROL POINT IN QUARRY | 579.797,000 | t Crushed stone | 0,000 | Public waterway | COD | 25,000 | 200 | ( mgO2/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 601 | 2.089 | 2023 | Quarry / SANITARY WATER CONTROL POINT IN QUARRY | 579.797,000 | t Crushed stone | 0,000 | Public waterway | DBO 5 | 5,000 | 60 | ( mgO2/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 602 | 2.089 | 2023 | Quarry / QUARRY / QUARRY TANK WATERS CONTROL POINT | 579.797,000 | t Crushed stone | 0,000 | Public waterway | pH | 8,600 | 6-9 | pH | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 603 | 2.089 | 2023 | Quarry / QUARRY / QUARRY TANK WATERS CONTROL POINT | 579.797,000 | t Crushed stone | 0,000 | Public waterway | Suspended matter | 4,000 | 90 | ( mg/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 604 | 2.089 | 2024 | Factory / CHECK POINT 1 PLUVIAL WATERS | 640.862,000 | t Product manufactured | 0,000 | Public waterway | pH | 8,410 | 5,5-9,5 | pH | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 605 | 2.089 | 2024 | Factory / CHECK POINT 1 PLUVIAL WATERS | 640.862,000 | t Product manufactured | 0,000 | Public waterway | Conductivity | 435,000 | 1.000 | ( μS/cm ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 606 | 2.089 | 2024 | Factory / CHECK POINT 1 PLUVIAL WATERS | 640.862,000 | t Product manufactured | 0,000 | Public waterway | Suspended matter | 16,000 | 50 | ( mg/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 607 | 2.089 | 2024 | Factory / CHECK POINT 1 PLUVIAL WATERS | 640.862,000 | t Product manufactured | 0,000 | Public waterway | COD | 14,000 | 100 | ( mgO2/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 608 | 2.089 | 2024 | Factory / CHECK POINT 1 PLUVIAL WATERS | 640.862,000 | t Product manufactured | 0,000 | Public waterway | Oils and fats | 0,500 | 10 | ( mg/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 609 | 2.089 | 2024 | Factory / CONTROL POINT 2 SANITARY WATERS | 640.862,000 | t Product manufactured | 0,000 | Public waterway | pH | 8,530 | 5,5-9,5 | pH | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 610 | 2.089 | 2024 | Factory / CONTROL POINT 2 SANITARY WATERS | 640.862,000 | t Product manufactured | 0,000 | Public waterway | Suspended matter | 28,000 | 60 | ( mg/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 611 | 2.089 | 2024 | Factory / CONTROL POINT 2 SANITARY WATERS | 640.862,000 | t Product manufactured | 0,000 | Public waterway | COD | 69,000 | 150 | ( mgO2/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 612 | 2.089 | 2024 | Factory / CONTROL POINT 2 SANITARY WATERS | 640.862,000 | t Product manufactured | 0,000 | Public waterway | DBO 5 | 35,000 | 90 | ( mgO2/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 613 | 2.089 | 2024 | Factory / CONTROL POINT 4 PLUVIAL WATERS | 640.862,000 | t Product manufactured | 0,000 | Public waterway | pH | 8,470 | 5,5-9,5 | pH | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 614 | 2.089 | 2024 | Factory / CONTROL POINT 4 PLUVIAL WATERS | 640.862,000 | t Product manufactured | 0,000 | Public waterway | Suspended matter | 29,000 | 50 | ( mg/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 615 | 2.089 | 2024 | Factory / CONTROL POINT 4 PLUVIAL WATERS | 640.862,000 | t Product manufactured | 0,000 | Public waterway | COD | 10,000 | 100 | ( mgO2/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 616 | 2.089 | 2024 | Factory / CONTROL POINT 4 PLUVIAL WATERS | 640.862,000 | t Product manufactured | 0,000 | Public waterway | Oils and fats | 0,500 | 10 | ( mg/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 617 | 2.089 | 2024 | Factory / CONTROL POINT 4 PLUVIAL WATERS | 640.862,000 | t Product manufactured | 0,000 | Public waterway | Hydrocarbons | 0,500 | 5 | ( mg/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 618 | 2.089 | 2024 | Factory / CHECK POINT 5 SANITARY WATERS | 640.862,000 | t Product manufactured | 0,000 | Public waterway | pH | 8,430 | 5,5-9,5 | pH | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 619 | 2.089 | 2024 | Factory / CHECK POINT 5 SANITARY WATERS | 640.862,000 | t Product manufactured | 0,000 | Public waterway | Suspended matter | 54,000 | 60 | ( mg/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 621 | 2.089 | 2024 | Factory / CHECK POINT 5 SANITARY WATERS | 640.862,000 | t Product manufactured | 0,000 | Public waterway | COD | 55,000 | 150 | ( mgO2/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 622 | 2.089 | 2024 | Factory / CHECK POINT 5 SANITARY WATERS | 640.862,000 | t Product manufactured | 0,000 | Public waterway | DBO 5 | 25,000 | 90 | ( mgO2/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 623 | 2.089 | 2024 | Quarry / SANITARY WATER CONTROL POINT IN QUARRY | 708.600,000 | t Crushed stone | 0,000 | Public waterway | pH | 8,270 | 6-9 | pH | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 624 | 2.089 | 2024 | Quarry / SANITARY WATER CONTROL POINT IN QUARRY | 708.600,000 | t Crushed stone | 0,000 | Public waterway | Suspended matter | 12,000 | 90 | ( mg/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 625 | 2.089 | 2024 | Quarry / SANITARY WATER CONTROL POINT IN QUARRY | 708.600,000 | t Crushed stone | 0,000 | Public waterway | COD | 21,000 | 200 | ( mgO2/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 626 | 2.089 | 2024 | Quarry / SANITARY WATER CONTROL POINT IN QUARRY | 708.600,000 | t Crushed stone | 0,000 | Public waterway | DBO 5 | 5,000 | 60 | ( mgO2/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 627 | 2.089 | 2024 | Quarry / QUARRY / QUARRY TANK WATERS CONTROL POINT | 708.600,000 | t Crushed stone | 0,000 | Public waterway | pH | 8,430 | 6-9 | pH | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 628 | 2.089 | 2024 | Quarry / QUARRY / QUARRY TANK WATERS CONTROL POINT | 708.600,000 | t Crushed stone | 0,000 | Public waterway | Suspended matter | 11,000 | 35 | ( mg/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 972 | 2.089 | 2025 | Factory / CHECK POINT 1 PLUVIAL WATERS | 645.674,000 | t Product manufactured | 0,000 | Public waterway | pH | 8,020 | 5,5-9,5 | pH | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 973 | 2.089 | 2025 | Factory / CHECK POINT 1 PLUVIAL WATERS | 645.674,000 | t Product manufactured | 0,000 | Public waterway | Conductivity | 560,000 | 1.000 | ( μS/cm ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 974 | 2.089 | 2025 | Factory / CHECK POINT 1 PLUVIAL WATERS | 645.674,000 | t Product manufactured | 0,000 | Public waterway | Suspended matter | 17,000 | 50 | ( mg/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 975 | 2.089 | 2025 | Factory / CHECK POINT 1 PLUVIAL WATERS | 645.674,000 | t Product manufactured | 0,000 | Public waterway | COD | 14,000 | 100 | ( mgO2/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 976 | 2.089 | 2025 | Factory / CHECK POINT 1 PLUVIAL WATERS | 645.674,000 | t Product manufactured | 0,000 | Public waterway | Oils and fats | 0,500 | 10 | ( mg/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 977 | 2.089 | 2025 | Factory / CONTROL POINT 2 SANITARY WATERS | 645.674,000 | t Product manufactured | 0,000 | Public waterway | pH | 8,240 | 5,5-9,5 | pH | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 978 | 2.089 | 2025 | Factory / CONTROL POINT 2 SANITARY WATERS | 645.674,000 | t Product manufactured | 0,000 | Public waterway | Suspended matter | 13,000 | 60 | ( mg/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 979 | 2.089 | 2025 | Factory / CONTROL POINT 2 SANITARY WATERS | 645.674,000 | t Product manufactured | 0,000 | Public waterway | COD | 19,000 | 150 | ( mgO2/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 980 | 2.089 | 2025 | Factory / CONTROL POINT 2 SANITARY WATERS | 645.674,000 | t Product manufactured | 0,000 | Public waterway | DBO 5 | 11,000 | 90 | ( mgO2/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 981 | 2.089 | 2025 | Factory / CONTROL POINT 4 PLUVIAL WATERS | 645.674,000 | t Product manufactured | 0,000 | Public waterway | pH | 8,270 | 5,5-9,5 | pH | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 982 | 2.089 | 2025 | Factory / CONTROL POINT 4 PLUVIAL WATERS | 645.674,000 | t Product manufactured | 0,000 | Public waterway | Suspended matter | 49,000 | 50 | ( mg/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 983 | 2.089 | 2025 | Factory / CONTROL POINT 4 PLUVIAL WATERS | 645.674,000 | t Product manufactured | 0,000 | Public waterway | COD | 10,000 | 100 | ( mgO2/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 984 | 2.089 | 2025 | Factory / CONTROL POINT 4 PLUVIAL WATERS | 645.674,000 | t Product manufactured | 0,000 | Public waterway | Oils and fats | 0,500 | 10 | ( mg/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 985 | 2.089 | 2025 | Factory / CONTROL POINT 4 PLUVIAL WATERS | 645.674,000 | t Product manufactured | 0,000 | Public waterway | Hydrocarbons | 0,500 | 5 | ( mg/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 986 | 2.089 | 2025 | Factory / CHECK POINT 5 SANITARY WATERS | 645.674,000 | t Product manufactured | 0,000 | Public waterway | pH | 8,560 | 5,5-9,5 | pH | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 987 | 2.089 | 2025 | Factory / CHECK POINT 5 SANITARY WATERS | 645.674,000 | t Product manufactured | 0,000 | Public waterway | Suspended matter | 14,000 | 60 | ( mg/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 988 | 2.089 | 2025 | Factory / CHECK POINT 5 SANITARY WATERS | 645.674,000 | t Product manufactured | 0,000 | Public waterway | DBO 5 | 6,000 | 90 | ( mgO2/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 989 | 2.089 | 2025 | Factory / CHECK POINT 5 SANITARY WATERS | 645.674,000 | t Product manufactured | 0,000 | Public waterway | COD | 20,000 | 150 | ( mgO2/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 990 | 2.089 | 2025 | Quarry / SANITARY WATER CONTROL POINT IN QUARRY | 663.668,000 | t Crushed stone | 0,000 | Public waterway | pH | 8,570 | 6-9 | pH | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 991 | 2.089 | 2025 | Quarry / QUARRY / QUARRY TANK WATERS CONTROL POINT | 663.668,000 | t Crushed stone | 0,000 | Public waterway | Suspended matter | 8,000 | 90 | ( mg/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 992 | 2.089 | 2025 | Quarry / SANITARY WATER CONTROL POINT IN QUARRY | 663.668,000 | t Crushed stone | 0,000 | Public waterway | COD | 10,000 | 200 | ( mgO2/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 993 | 2.089 | 2025 | Quarry / SANITARY WATER CONTROL POINT IN QUARRY | 663.668,000 | t Crushed stone | 0,000 | Public waterway | DBO 5 | 5,000 | 60 | ( mgO2/l ) | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 994 | 2.089 | 2025 | Quarry / QUARRY / QUARRY TANK WATERS CONTROL POINT | 663.668,000 | t Crushed stone | 0,000 | Public waterway | pH | 8,440 | 6-9 | pH | 0,000 | 138.963 | 2.089 | ||
| VALIDATED | 995 | 2.089 | 2025 | Quarry / QUARRY / QUARRY TANK WATERS CONTROL POINT | 663.668,000 | t Crushed stone | 0,000 | Public waterway | Suspended matter | 27,000 | 35 | ( mg/l ) | 0,000 | 138.963 | 2.089 | ||
| state | wdt_ID | userid | Year | Center | Unit | Destination | Pollutant | ||||||||||
| ∑ = 46,237,189.000 |
 |
Atmospheric emissions |
Emissions management
Particulates and combustion gases are the most characteristic atmospheric emissions of our activity. Emissions generated during the handling, transport, storage and treatment of powdery materials are emitted through channeled and diffuse sources, while combustion gases are emitted through the kiln chimneys, the most characteristic compounds emitted beingCO2, NOx and SO2, together with other minor pollutants. The emission of pollutants is monitored by ECAMATs (Entities Accredited by the Government of Cantabria for Environmental Monitoring) or the continuous systems installed in the factory chimneys, following the requirements of an Environmental Monitoring Plan that complies with the Integrated Environmental Authorization.
Environmental management and control
At the Mataporquera plant, seven emission sources are monitored via chimneys: two from the clinker manufacturing process and the cooling kiln, and the rest from the fuel grinding, cement grinding, stone crushing, and cement and mortar bagging processes. All of these are equipped with baghouse filtration systems, which represent some of the Best Available Techniques in the industry. Furthermore, three of them—the kilns, the cooler, and the cement mill—are equipped with continuous particle measurement systems; in the case of the kiln, they also measure flue gas emissions of NOx, SO₂, CO, and TOC. Particulate emissions continue to be considered a significant environmental concern, and multi-year measures have been established to reduce the level of settleable particulates in the surrounding area. Notable actions include replacing the filter in the cooler and changing 1,360 filter bags in the cement mill. In 2025, there were no instances of localized sources exceeding the atmospheric emission limit value. Emission levels at the main sources—the kiln, cement mill, and cooler—remained consistent with previous years. In the combustion process that takes place in the kiln for clinker production, mainly carbon dioxide, sulfur dioxide and nitrogen oxides are generated, together with other minority pollutants: HCl, Hf, total organic compounds, heavy metals and dioxins and furans. Combustion gas emission values comply with the legal limits established in the Integrated Environmental Authorization. Continuously measured emissions of the main pollutants SO2 and NOx remain constant compared to previous years. A 40-90% reduction in the emission of these pollutants has been achieved since the Integrated Environmental Authorization was obtained in July 2005. The use of alternative fuels has been the cause of the decrease in SO2 and NOx emissions. In the case of SO2, this is due to the reduction in the clinker kiln's contribution, and in the case of NOx, it is caused by the effect on the thermal balance in the kiln due to the mix of fuels with different calorific power. The minimization of emissions resulting from the transfer and movement of powdery materials has been achieved by adopting a series of preventive measures such as paving in circulation areas, conveyor belt fairings, suction devices at transfer, loading and unloading points, wind protection screens and road watering, among others. For the inspection of air quality, a PM10, NOx, SO2 immission campaign was carried out in the Valdeolea Town Hall square, which is complemented with those carried out by the Autonomous Administration in order to control the air quality of the environment in all its emission sources, confined and diffuse, as well as the possible migration of pollutants from emission sources in nearby towns. Additionally, other sedimentable particles campaigns were carried out; one in the factory and two in the quarry for one month. All controls gave results below the legal reference values. The tables show the highest value measured for its impact on the perception of particles in the environment. Emission levels of minority gas pollutants have been maintained at values below the legal limits. It should be noted that data on 37 pollutants are reported annually to the State Registry of Emissions and Pollutant Sources (PRTR Spain) in the form of pollutant loads from piped emissions. In 2025, CO andNOx were the only pollutants whose pollutant loads exceeded the reporting threshold.Emissions from channeled sources
Particulate matter emission
Emission of combustion gases
Diffuse source emissions
Other emissions
| state | wdt_ID | userid | Year | Centre/Focus | Units Pr. | Unit | Origin/Type | Pollutant | Concentration | Conc. unit | Limit | Mass emission (kg) | ID | post_author | Ratio (kgUnits Pr. |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| VALIDATED | 344 | 2.089 | 2023 | Factory | 367.612,000 | t Product manufactured | Vehicle emission source | HCl | 1,910 | (mg/Nm3) | 10 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 345 | 2.089 | 2023 | Factory | 367.612,000 | t Product manufactured | Vehicle emission source | HF | 0,020 | (mg/Nm3) | 1 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 346 | 2.089 | 2023 | Factory | 367.612,000 | t Product manufactured | Vehicle emission source | COT | 25,000 | (mg/Nm3) | 50 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 347 | 2.089 | 2023 | Factory | 367.612,000 | t Product manufactured | Vehicle emission source | Hg | 0,007 | (mg/Nm3) | 0,05 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 348 | 2.089 | 2023 | Factory | 367.612,000 | t Product manufactured | Vehicle emission source | Cd + Tl | 0,003 | (mg/Nm3) | 0,05 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 349 | 2.089 | 2023 | Factory | 367.612,000 | t Product manufactured | Vehicle emission source | Sb + As + Pb + Cr + Co + Cu + NI + Mn + V | 0,024 | (mg/Nm3) | 0,5 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 350 | 2.089 | 2023 | Factory | 367.612,000 | t Product manufactured | Vehicle emission source | Dioxins and Furans | 0,026 | (ng/Nm3) | 0,1 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 351 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | Vehicle emission source | HCl | 2,890 | (mg/Nm3) | 10 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 352 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | Vehicle emission source | HF | 0,046 | (mg/Nm3) | 1 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 353 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | Vehicle emission source | COT | 32,600 | (mg/Nm3) | 120 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 354 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | Vehicle emission source | Hg | 0,003 | (mg/Nm3) | 0,05 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 355 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | Vehicle emission source | Cd + Tl | 0,014 | (mg/Nm3) | 0,05 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 366 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | Vehicle emission source | Dioxins and Furans | 0,028 | (ng/Nm3) | 0,1 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 368 | 2.089 | 2023 | Factory | 367.612,000 | t Clinker fabricated | Vehicle emission source | Particulate matter emissions | 10,200 | (mg/Nm3) | 20 | 10.163,000 | 138.963 | 2.089 | 0,028 |
| VALIDATED | 369 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | Vehicle emission source | Particulate emissions from the furnace | 9,900 | (mg/Nm3) | 20 | 13.115,100 | 138.963 | 2.089 | 0,033 |
| VALIDATED | 372 | 2.089 | 2023 | Factory | 367.612,000 | t Clinker fabricated | Vehicle emission source | NOx | 183,200 | (mg/Nm3) | 500 | 182.528,000 | 138.963 | 2.089 | 0,497 |
| VALIDATED | 373 | 2.089 | 2023 | Factory | 367.612,000 | t Clinker fabricated | Vehicle emission source | SO2 | 19,400 | (mg/Nm3) | 400 | 19.323,000 | 138.963 | 2.089 | 0,053 |
| VALIDATED | 374 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | Vehicle emission source | NOx | 175,600 | (mg/Nm3) | 500 | 232.627,900 | 138.963 | 2.089 | 0,584 |
| VALIDATED | 375 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | Vehicle emission source | SO2 | 15,900 | (mg/Nm3) | 400 | 21.063,700 | 138.963 | 2.089 | 0,053 |
| VALIDATED | 377 | 2.089 | 2023 | Factory | 628.160,000 | t Product manufactured | Diffuse emissions | Measurement of settleable particles | 125,400 | (mg/m2 day) | 300 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 378 | 2.089 | 2023 | Quarry | 579.797,000 | t Crushed stone | Diffuse emissions | Measurement of settleable particles | 107,400 | (mg/m2 day) | 300 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 380 | 2.089 | 2024 | Factory | 640.862,000 | t Product manufactured | Diffuse emissions | Measurement of settleable particles P1. INPUT | 23,100 | (mg/m2 day) | 300 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 381 | 2.089 | 2024 | Quarry | 708.600,000 | t Crushed stone | Diffuse emissions | Measurement of sedimentable particles P2. QUARRY | 173,600 | (mg/m2 day) | 300 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 389 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | Vehicle emission source | Sb + As + Pb + Cr + Co + Cu + NI + Mn + V | 0,053 | (mg/Nm3) | 0,5 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 486 | 2.089 | 2023 | Factory | 367.612,000 | t Clinker fabricated | Vehicle emission source | Particulate matter emissions COOLER | 8,900 | (mg/Nm3) | 20 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 487 | 2.089 | 2023 | Factory | 628.160,000 | t Clinker fabricated | Vehicle emission source | Particulate Matter Emissions CEMENT MILL | 7,300 | (mg/Nm3) | 20 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 488 | 2.089 | 2023 | Factory | 15.644,000 | t coke and ground coal | Vehicle emission source | Particulate matter emissions MOLINO CARBÓN | 8,900 | (mg/Nm3) | 20 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 489 | 2.089 | 2023 | Quarry | 579.797,000 | t Crushed stone | Vehicle emission source | Particulate Matter Emissions QUARRY CRUSHING PLANT | 0,900 | (mg/Nm3) | 20 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 490 | 2.089 | 2023 | Factory | 53.608,000 | t Manufactured mortar | Vehicle emission source | Particulate matter emissions MORTAR SACKING | 1,500 | (mg/Nm3) | 20 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 492 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | Vehicle emission source | Particulate matter emissions COOLER | 8,700 | (mg/Nm3) | 20 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 493 | 2.089 | 2024 | Factory | 582.772,000 | t Cement manufactured | Vehicle emission source | Particulate Matter Emissions CEMENT MILL | 10,500 | (mg/Nm3) | 20 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 494 | 2.089 | 2024 | Factory | 15.417,000 | t coke and ground coal | Vehicle emission source | Particulate matter emissions MOLINO CARBÓN | 16,400 | (mg/Nm3) | 20 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 495 | 2.089 | 2024 | Quarry | 708.600,000 | t Crushed stone | Vehicle emission source | Particulate Matter Emissions QUARRY CRUSHING PLANT | 3,700 | (mg/Nm3) | 10 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 496 | 2.089 | 2024 | Factory | 58.090,000 | t Manufactured mortar | Vehicle emission source | Particulate matter emissions MORTAR SACKING | 6,600 | (mg/Nm3) | 10 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 735 | 2.089 | 2025 | Factory | 433.549,000 | t Clinker fabricated | Vehicle emission source | HCl | 1,240 | (mg/Nm3) | 10 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 736 | 2.089 | 2025 | Factory | 433.549,000 | t Clinker fabricated | Vehicle emission source | HF | 0,039 | (mg/Nm3) | 1 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 737 | 2.089 | 2025 | Factory | 433.549,000 | t Clinker fabricated | Vehicle emission source | Hg | 0,003 | (mg/Nm3) | 0,05 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 738 | 2.089 | 2025 | Factory | 433.549,000 | t Clinker fabricated | Vehicle emission source | Cd + Tl | 0,008 | (mg/Nm3) | 0,05 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 739 | 2.089 | 2025 | Factory | 433.549,000 | t Clinker fabricated | Vehicle emission source | Dioxins and Furans | 0,031 | (ng/Nm3) | 0,1 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 741 | 2.089 | 2025 | Factory | 20.582,400 | t coke and ground coal | Vehicle emission source | Particulate matter emissions MOLINO CARBÓN | 2,750 | (mg/Nm3) | 20 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 742 | 2.089 | 2025 | Quarry | 663.668,000 | t Crushed stone | Vehicle emission source | Particulate Matter Emissions QUARRY CRUSHING PLANT | 1,440 | (mg/Nm3) | 10 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 743 | 2.089 | 2025 | Factory | 63.831,000 | t Manufactured mortar | Vehicle emission source | Particulate matter emissions MORTAR SACKING | 4,380 | (mg/Nm3) | 10 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 769 | 2.089 | 2025 | Factory | 433.549,000 | t Clinker fabricated | Vehicle emission source | Particulate emissions from the furnace | 9,660 | (mg/Nm3) | 20 | 13.282,700 | 138.963 | 2.089 | 0,031 |
| VALIDATED | 770 | 2.089 | 2025 | Factory | 433.549,000 | t Clinker fabricated | Vehicle emission source | Particulate matter emissions COOLER | 4,100 | (mg/Nm3) | 20 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 771 | 2.089 | 2025 | Factory | 581.843,000 | t Cement manufactured | Vehicle emission source | Particulate Matter Emissions CEMENT MILL | 9,200 | (mg/Nm3) | 20 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 772 | 2.089 | 2025 | Factory | 433.549,000 | t Clinker fabricated | Vehicle emission source | COT | 34,800 | (mg/Nm3) | 120 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 773 | 2.089 | 2025 | Factory | 433.549,000 | t Clinker fabricated | Vehicle emission source | Sb + As + Pb + Cr + Co + Cu + Ni + Mn + V | 0,094 | (mg/Nm3) | 0,5 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 774 | 2.089 | 2025 | Quarry | 663.668,000 | t Crushed stone | Diffuse emissions | Measurement of sedimentable particles P2. QUARRY | 109,700 | (mg/m2 day) | 300 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 775 | 2.089 | 2025 | Factory | 645.674,000 | t Product manufactured | Diffuse emissions | Measurement of settleable particles P1. FACTORY INPUT | 182,800 | (mg/m2 day) | 300 | 138.963 | 2.089 | 0,000 | |
| VALIDATED | 776 | 2.089 | 2025 | Factory | 433.549,000 | t Clinker fabricated | Vehicle emission source | NOx | 198,300 | (mg/Nm3) | 500 | 272.600,900 | 138.963 | 2.089 | 0,629 |
| VALIDATED | 777 | 2.089 | 2025 | Factory | 433.459,000 | t Clinker fabricated | Vehicle emission source | SO2 | 7,700 | (mg/Nm3) | 400 | 10.515,100 | 138.963 | 2.089 | 0,024 |
| state | wdt_ID | userid | Year | Centre/Focus | Unit | Origin/Type | Pollutant | ID | post_author | ||||||
| ∑ = 21,033,546.400 |
 |
CO2 emissions |
Confined greenhouse gas emissions
In 2025, 313,978 tons ofCO2 were emitted into the atmosphere, resulting from the decarbonation of limestone—through the transformation of limestone into calcium oxide at the high temperatures of the process —and the combustion process—through the oxidation of carbon in fuels in the presence of oxygen—which amounted to 724 kgCO2 per ton of clinker.
The increase in emissions in absolute terms is a direct result of the increase in production. However, the decrease in specificCO2 emissions is significant, thanks to improved furnace energy efficiency and the increased use of biomass and decarbonized material.
TheCO2 allowance for 2025 has remained at 312,098 metric tons ofCO2, which corresponds to 100% of the activity level reference value (HAL).
Note: The "Scope 1" designation refers only to direct emissions verified for the CO2 market (ETS).
CO₂ emissions per center.
GHG calculated
| wdt_ID | userid | Year | Center | Units Pr. | Units | Origin/Type | CO2eq Direct (S1) | CO2eq Indirect (S2) | CO2eq Indirect (S3) | CO2eq Saved/Compensated | ID | post_author | Category GHG (S3) | T CO2eq Total | TotalUnits Pr. | IndirectUnits ratio | DirectUnits ratio | Ratio of CO2eq Savings toUnits Pr. |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| 235 | 2.089 | 2023 | Factory | 367.612,000 | t Clinker fabricated | MMPP decarbonation | 183.903,000 | 138.963 | 2.089 | 183.903,000 | 0,500264 | 0,000000 | 0,500264 | 0,000000 | ||||
| 306 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | CO2 Renewable electricity consumption, energy supplier, and PPAs | 0,000 | 0,000 | 0,000 | -14.860,400 | 138.963 | 2.089 | 0,000 | 0,000000 | 0,000000 | 0,000000 | 0,037303 | |
| 307 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | Replacement of fossil fuels | 0,000 | 0,000 | 0,000 | -27.823,643 | 138.963 | 2.089 | 0,000 | 0,000000 | 0,000000 | 0,000000 | 0,069843 | |
| 800 | 2.089 | 2025 | Factory | 433.459,000 | t Clinker fabricated | Fossil fuels | 214.890,000 | 138.963 | 2.089 | 214.890,000 | 0,495756 | 0,000000 | 0,495756 | 0,000000 | ||||
| 806 | 2.089 | 2025 | Factory | 433.549,000 | t Clinker fabricated | Replacement of fossil fuels | 0,000 | 0,000 | 0,000 | -31.273,000 | 138.963 | 2.089 | 0,000 | 0,000000 | 0,000000 | 0,000000 | 0,072133 | |
| 807 | 2.089 | 2025 | Factory | 433.549,000 | t Clinker fabricated | CO2 Renewable electricity consumption, energy supplier, and PPAs | 0,000 | 0,000 | 0,000 | -13.164,990 | 138.963 | 2.089 | 0,000 | 0,000000 | 0,000000 | 0,000000 | 0,030366 | |
| 808 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | MMPP decarbonation | 199.865,000 | 138.963 | 2.089 | 199.865,000 | 0,501704 | 0,000000 | 0,501704 | 0,000000 | ||||
| 822 | 2.089 | 2025 | Factory | 433.549,000 | t Clinker fabricated | Replacement of fossil fuels | 99.087,690 | 0,000 | 0,000 | 138.963 | 2.089 | 99.087,690 | 0,228550 | 0,000000 | 0,228550 | 0,000000 | ||
| 823 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | Replacement of fossil fuels | 92.412,050 | 0,000 | 0,000 | 138.963 | 2.089 | 92.412,050 | 0,231974 | 0,000000 | 0,231974 | 0,000000 | ||
| 824 | 2.089 | 2023 | Factory | 367.612,000 | t Clinker fabricated | Replacement of fossil fuels | 88.839,170 | 0,000 | 0,000 | 138.963 | 2.089 | 88.839,170 | 0,241666 | 0,000000 | 0,241666 | 0,000000 | ||
| 825 | 2.089 | 2023 | Factory | t Clinker fabricated | Replacement of fossil fuels | 0,000 | 0,000 | 0,000 | -27.124,000 | 138.963 | 2.089 | 0,000 | 0,000000 | 0,000000 | 0,000000 | 0,000000 | ||
| 826 | 2.089 | 2023 | Factory | 367,612 | t Clinker fabricated | CO2 Renewable electricity consumption, energy supplier, and PPAs | 0,000 | 0,000 | 0,000 | -11.819,970 | 138.963 | 2.089 | 0,000 | 0,000000 | 0,000000 | 0,000000 | 32,153385 | |
| wdt_ID | userid | Year | Center | Units Pr. | Units | Origin/Type | ID | post_author | Category GHG (S3) |
 |
Waste production and management |
GenerWaste generation
The cement manufacturing process does not give rise to the generation of waste, which is derived from facility maintenance activities, construction work and building cleaning, among others. The management criteria established are based on minimization in the generation process, reuse and recycling, with internal segregation and appropriate external management for each type of waste. The material generated during maintenance of the interior of the kiln and tower, as well as during the cleaning of facilities and access roads, is reused as raw material for clinker production, as it consists of a mixture of the raw materials used in the clinker and cement manufacturing processes. The Integrated Environmental Permit establishes reference quantities for each type of waste generated. In 2025, the quantities of scrap metal (254,230 metric tons generated compared to the 200,000 metric tons specified in the Permit) and wood (47.96 metric tons compared to 40 metric tons) were exceeded due to the waste generated by the September fire. The reference value for paper and cardboard (48.84 metric tons versus 40 metric tons) was also exceeded due to the disposal of obsolete cement bags from the bagging facility, which has been inactive since 2016. Refractory brick also exceeded the threshold (92.02 metric tons compared to 40 metric tons) due to the removal of obsolete material from the warehouses. Aqueous cleaning fluids, which also exceed the reference value, are used in the auto repair shop to clean parts during maintenance work. Looking ahead to 2024, there is also an increase in the amount of waste sent to landfills, driven by the disposal of replaced filter bags from the cooler and cement filters, as well as debris from the September fire. Theremaining waste is delivered to an authorized waste management company with which a treatment contract has been established, and each delivery is documented as required by law
Environmental management and control
The waste minimization measures described in the 2022 EMAS Environmental Statement include the modification of the management system for rags generated in maintenance operations, changing to a system of rags for rent that are collected separately and, after an authorized cleaning process, are reused in our activities.
In 2026, there will be an increase in the generation of Hazardous waste Hazardous two unusual circumstances: First, the managed cloth rental system has been suspended because it did not meet the required quality specifications. On the other hand, predictive maintenance operations will be carried out on the clinker kiln filter in the coming years, which will also increase the number of filter bags managed as Hazardous waste.
In an effort to minimize Hazardous waste, Hazardous continuing with the project to reduce used oil. Once the Integrated Environmental Permit for this new Recovery has been obtained, we expect to secure the greenhouse gas emissions permit in 2026, prior to the revision of the Monitoring Plan.
Follow-up of the waste minimization plan
In 2025, the reduction in Hazardous waste generation continued; 16,688 tons were generated this year, compared to 21,037 tons in 2024 and 30,426 tons in 2023. This decrease was due to a reduction in the generation of contaminated soil resulting from spill cleanup operations. In 2025, the rest of the waste was generated in typical quantities, and the management system for rags impregnated with hazardous substances continued.
In the case of Hazardous waste, excluding plant material reused by the quarry for clinker production, 331.04 tons were generated in 2024, compared to 203.23 tons in 2023. The increase in the generation of wood, scrap metal, and waste sent to landfills was driven by waste management following the fire at the storage and dosing facility for solid alternative fuels for the main burner.
Recovery . Recovery of Hazardous waste Hazardous 49.8% of Hazardous waste were sent for recycling and Recovery .
It is important to note that all Hazardous waste Hazardous generated during corrective or preventive maintenance activities or as part of general repairs.
If the material reused in clinker production is not taken into account, the amount of waste generated is 2% higher than the limits set in the Integrated Environmental Permit due to waste generated by the fire, the emptying of the bagged material storage area, and obsolete refractory bricks .
-
- Hazardous(125,925 kg AAI) 16,688 kg (-86%)
- Hazardous (355,800 kg AAI) 484,990 kg (+36%)
- Total(490,225 kg AAI) 501,678 kg (+2%)
Evolution of specific metrics and ratios
Generación de residuos
Destination of waste
Type and destination
| wdt_ID | userid | Year | Center | Units Pr. | Units | Non Hazardous | Hazardous | Disposal/ Controlled landfill | Other treatments | Recovery | By-products | post_author | NP Ratio (kg)Units Pr. | RP Ratio (kg)Units Pr. | Totals (t) | Total ratio (t)Units Pr. |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| 96 | 2.089 | 2023 | Factory and Quarry | 628.160,000 | t Product manufactured | 2.273,420 | 30,430 | 35,061 | 2.268,789 | 2.089 | 3,619 | 0,04844307183 | 2.303,85 | 0,003667616531 | ||
| 97 | 2.089 | 2024 | Factory and Quarry | 640.862,000 | t Product manufactured | 4.933,000 | 21,037 | 36,164 | 4.917,873 | 2.089 | 7,697 | 0,03282609985 | 4.954,04 | 0,007730271104 | ||
| 157 | 2.089 | 2025 | Factory and Quarry | 645.674,000 | t Product manufactured | 1.481,120 | 16,688 | 46,003 | 1.451,810 | 2.089 | 2,294 | 0,02584586029 | 1.497,81 | 0,002319758888 | ||
| wdt_ID | userid | Year | Center | Units | post_author | |||||||||||
| ∑ = 1,914,696.000 |
List of waste
| wdt_ID | userid | Year | Center | Units Pr. | Units | Description of the waste | CER/LER code. | Treatment | Hazardous | Quantity (t) | post_author | Ratio quantity (t)/pdU. |
|---|---|---|---|---|---|---|---|---|---|---|---|---|
| 1.531 | 2.089 | 2023 | Factory and Quarry | 628.160,000 | t Product manufactured | Scrap | 200140 | R4 | No | 130,500 | 2.089 | 0,000207749618 |
| 1.532 | 2.089 | 2023 | Factory and Quarry | 628.160,000 | t Product manufactured | Mixing of non-recoverable waste | 191212 | D5 | No | 10,160 | 2.089 | 0,000016174223 |
| 1.533 | 2.089 | 2023 | Factory and Quarry | 628.160,000 | t Product manufactured | Wood | 200138 | R12 | No | 44,900 | 2.089 | 0,000071478604 |
| 1.534 | 2.089 | 2023 | Factory and Quarry | 628.160,000 | t Product manufactured | Paper and Cardboard | 200101 | R12 | No | 5,840 | 2.089 | 0,000009296994 |
| 1.535 | 2.089 | 2023 | Factory and Quarry | 628.160,000 | t Product manufactured | Industrial inerts | - | R5 Recovery | No | 2.069,740 | 2.089 | 0,003294924860 |
| 1.536 | 2.089 | 2023 | Factory and Quarry | 628.160,000 | t Product manufactured | WWTP sludge | 200304 | D9 | No | 9,620 | 2.089 | 0,000015314570 |
| 1.537 | 2.089 | 2023 | Factory and Quarry | 628.160,000 | t Product manufactured | Plastic | 200139 | R12 | No | 2,660 | 2.089 | 0,000004234590 |
| 1.551 | 2.089 | 2023 | Factory and Quarry | 628.160,000 | t Product manufactured | Engine oil | 130208 | R13 | Yes | 11,160 | 2.089 | 0,000017766174 |
| 1.552 | 2.089 | 2023 | Factory and Quarry | 628.160,000 | t Product manufactured | Fats | 120112 | D15 | Yes | 0,780 | 2.089 | 0,000001241722 |
| 1.553 | 2.089 | 2023 | Factory and Quarry | 628.160,000 | t Product manufactured | Fuel blend residues | - | - | Yes | 0,000 | 2.089 | 0,000000000000 |
| 1.554 | 2.089 | 2023 | Factory and Quarry | 628.160,000 | t Product manufactured | Non-halogenated cleaning solvent | 140603 | R13 | Yes | 0,605 | 2.089 | 0,000000963130 |
| 1.555 | 2.089 | 2023 | Factory and Quarry | 628.160,000 | t Product manufactured | Contaminated packaging | 150110 | R13 | Yes | 1,360 | 2.089 | 0,000002165053 |
| 1.556 | 2.089 | 2023 | Factory and Quarry | 628.160,000 | t Product manufactured | Absorbent material (filter sleeves) | 150202 | D15 | Yes | 3,500 | 2.089 | 0,000005571829 |
| 1.557 | 2.089 | 2023 | Factory and Quarry | 628.160,000 | t Product manufactured | Mix of lamps | 200121 | R4 | Yes | 0,132 | 2.089 | 0,000000210138 |
| 1.558 | 2.089 | 2023 | Factory and Quarry | 628.160,000 | t Product manufactured | Batteries | 200133 | R12 | Yes | 0,068 | 2.089 | 0,000000108253 |
| 1.559 | 2.089 | 2023 | Factory and Quarry | 628.160,000 | t Product manufactured | First aid kit waste | 180103 | D9 | Yes | 0,001 | 2.089 | 0,000000001592 |
| 1.560 | 2.089 | 2023 | Factory and Quarry | 628.160,000 | t Product manufactured | Electrical and electronic equipment | 160213 | R13 | Yes | 1,760 | 2.089 | 0,000002801834 |
| 1.561 | 2.089 | 2023 | Factory and Quarry | 628.160,000 | t Product manufactured | Oil filters | 160107 | R13 | Yes | 0,060 | 2.089 | 0,000000095517 |
| 1.562 | 2.089 | 2023 | Factory and Quarry | 628.160,000 | t Product manufactured | Contaminated land | 150202 | D9 | Yes | 9,800 | 2.089 | 0,000015601121 |
| 1.563 | 2.089 | 2023 | Factory and Quarry | 628.160,000 | t Product manufactured | Aqueous cleaning liquid | 120301 | D9 | Yes | 1,200 | 2.089 | 0,000001910341 |
| 1.564 | 2.089 | 2024 | Factory and Quarry | 640.862,000 | t Product manufactured | Wood | 150103 | R12 | No | 35,540 | 2.089 | 0,000055456557 |
| 1.565 | 2.089 | 2024 | Factory and Quarry | 640.862,000 | t Product manufactured | Paper and Cardboard | 150101 | R12 | No | 6,920 | 2.089 | 0,000010797957 |
| 1.566 | 2.089 | 2024 | Factory and Quarry | 640.862,000 | t Product manufactured | Scrap | 170407 | R4 | No | 257,580 | 2.089 | 0,000401927404 |
| 1.567 | 2.089 | 2024 | Factory and Quarry | 640.862,000 | t Product manufactured | Plastic | 150102 | R12 | No | 1,440 | 2.089 | 0,000002246974 |
| 1.568 | 2.089 | 2024 | Factory and Quarry | 640.862,000 | t Product manufactured | Mixing of non-recoverable waste | 191212 | D5 | No | 19,840 | 2.089 | 0,000030958303 |
| 1.569 | 2.089 | 2024 | Factory and Quarry | 640.862,000 | t Product manufactured | WWTP sludge | 200304 | D9 | No | 10,660 | 2.089 | 0,000016633846 |
| 1.570 | 2.089 | 2024 | Factory and Quarry | 640.862,000 | t Product manufactured | Glass | 200102 | R12 | No | 0,060 | 2.089 | 0,000000093624 |
| 1.572 | 2.089 | 2024 | Factory and Quarry | 640.862,000 | t Product manufactured | Industrial inerts | - | R5 Recovery | No | 4.600,560 | 2.089 | 0,007178706180 |
| 1.573 | 2.089 | 2024 | Factory and Quarry | 640.862,000 | t Product manufactured | RAOS WWTP sludge | 200304 | D9 | No | 0,400 | 2.089 | 0,000000624159 |
| 1.574 | 2.089 | 2024 | Factory and Quarry | 640.862,000 | t Product manufactured | Non-halogenated cleaning solvent | 140603 | R13 | Yes | 2,245 | 2.089 | 0,000003503094 |
| 1.575 | 2.089 | 2024 | Factory and Quarry | 640.862,000 | t Product manufactured | Aqueous cleaning liquid | 120301 | D15 | Yes | 1,200 | 2.089 | 0,000001872478 |
| 1.576 | 2.089 | 2024 | Factory and Quarry | 640.862,000 | t Product manufactured | First aid kit waste | 180103 | D9 | Yes | 0,004 | 2.089 | 0,000000006242 |
| 1.577 | 2.089 | 2024 | Factory and Quarry | 640.862,000 | t Product manufactured | Engine oil | 130208 | R1302 | Yes | 10,600 | 2.089 | 0,000016540222 |
| 1.578 | 2.089 | 2024 | Factory and Quarry | 640.862,000 | t Product manufactured | Mix of lamps | 200121 | R12 | Yes | 0,318 | 2.089 | 0,000000496207 |
| 1.579 | 2.089 | 2024 | Factory and Quarry | 640.862,000 | t Product manufactured | Absorbent material (filter sleeves) | 150202 | D15 | Yes | 1,560 | 2.089 | 0,000002434221 |
| 1.580 | 2.089 | 2024 | Factory and Quarry | 640.862,000 | t Product manufactured | Oil filters | 160107 | R13 | Yes | 0,720 | 2.089 | 0,000001123487 |
| 1.581 | 2.089 | 2024 | Factory and Quarry | 640.862,000 | t Product manufactured | Contaminated packaging | 150110 | R13 | Yes | 0,780 | 2.089 | 0,000001217111 |
| 1.582 | 2.089 | 2024 | Factory and Quarry | 640.862,000 | t Product manufactured | Lead batteries | 160106 | R13 | Yes | 0,170 | 2.089 | 0,000000265268 |
| 1.583 | 2.089 | 2024 | Factory and Quarry | 640.862,000 | t Product manufactured | Contaminated land | 150202 | D1501 | Yes | 1,717 | 2.089 | 0,000002679204 |
| 1.584 | 2.089 | 2024 | Factory and Quarry | 628.160,000 | t Product manufactured | Fats | 120112 | D1501 | Yes | 0,783 | 2.089 | 0,000001246498 |
| 1.585 | 2.089 | 2024 | Factory and Quarry | 628.160,000 | t Product manufactured | Electrical and electronic equipment | 160213 | R13 | Yes | 0,940 | 2.089 | 0,000001496434 |
| 2.452 | 2.089 | 2025 | Factory and Quarry | 645.674,000 | t Product manufactured | Wood | 150103 | R12 | No | 47,960 | 2.089 | 0,000074278971 |
| 2.453 | 2.089 | 2025 | Factory and Quarry | 645.674,000 | t Product manufactured | Paper and Cardboard | 150101 | R12 | No | 48,840 | 2.089 | 0,000075641887 |
| 2.454 | 2.089 | 2025 | Factory and Quarry | 645.674,000 | t Product manufactured | Scrap | 170407 | R4 | No | 254,230 | 2.089 | 0,000393743592 |
| 2.455 | 2.089 | 2025 | Factory and Quarry | 645.674,000 | t Product manufactured | Plastic | 150102 | R12 | No | 1,940 | 2.089 | 0,000003004612 |
| 2.456 | 2.089 | 2025 | Factory and Quarry | 645.674,000 | t Product manufactured | Mixing of non-recoverable waste | 191212 | D5 | No | 27,700 | 2.089 | 0,000042900907 |
| 2.457 | 2.089 | 2025 | Factory and Quarry | 645.674,000 | t Product manufactured | WWTP sludge | 200304 | D9 | No | 12,180 | 2.089 | 0,000018864009 |
| 2.458 | 2.089 | 2025 | Factory and Quarry | 645.674,000 | t Product manufactured | Glass | 200102 | R12 | No | 0,120 | 2.089 | 0,000000185852 |
| 2.459 | 2.089 | 2025 | Factory and Quarry | 645.674,000 | t Product manufactured | Refractory brick | No | 92,020 | 2.089 | 0,000142517741 | ||
| 2.460 | 2.089 | 2025 | Factory and Quarry | 645.674,000 | t Product manufactured | Industrial inerts | - | R5 Recovery | No | 996,130 | 2.089 | 0,001542775456 |
| 2.461 | 2.089 | 2025 | Factory and Quarry | 645.674,000 | t Product manufactured | Engine oil | 130208 | R1302 | Yes | 5,520 | 2.089 | 0,000008549206 |
| 2.462 | 2.089 | 2025 | Factory and Quarry | 645.674,000 | t Product manufactured | Fats | 120112 | D1501 | Yes | 0,660 | 2.089 | 0,000001022188 |
| 2.463 | 2.089 | 2025 | Factory and Quarry | 645.674,000 | t Product manufactured | Non-halogenated cleaning solvent | 140603 | R13 | Yes | 2,580 | 2.089 | 0,000003995825 |
| 2.464 | 2.089 | 2025 | Factory and Quarry | 645.674,000 | t Product manufactured | Cleaning fluids | 120301 | D9 | Yes | 0,355 | 2.089 | 0,000000549813 |
| 2.465 | 2.089 | 2025 | Factory and Quarry | 645.674,000 | t Product manufactured | Contaminated packaging | 150110 | R13 | Yes | 0,660 | 2.089 | 0,000001022188 |
| 2.466 | 2.089 | 2025 | Factory and Quarry | 645.674,000 | t Product manufactured | Absorbent material (filter sleeves) | 150202 | D15 | Yes | 2,920 | 2.089 | 0,000004522406 |
| 2.467 | 2.089 | 2025 | Factory and Quarry | 645.674,000 | t Product manufactured | Aqueous liquid | 120301 | D15 | Yes | 0,900 | 2.089 | 0,000001393892 |
| 2.468 | 2.089 | 2025 | Factory and Quarry | 645.674,000 | t Product manufactured | Mix of lamps | 200121 | R12 | Yes | 0,090 | 2.089 | 0,000000139389 |
| 2.469 | 2.089 | 2025 | Factory and Quarry | 645.674,000 | t Product manufactured | Oil filters | 160107 | R13 | Yes | 0,500 | 2.089 | 0,000000774385 |
| 2.470 | 2.089 | 2025 | Factory and Quarry | 645.674,000 | t Product manufactured | First aid kit waste | 180103 | D9 | Yes | 0,003 | 2.089 | 0,000000004646 |
| 2.471 | 2.089 | 2025 | Factory and Quarry | 645.674,000 | t Product manufactured | Electrical and electronic equipment | 160213 | R13 | Yes | 0,860 | 2.089 | 0,000001331942 |
| 2.472 | 2.089 | 2025 | Factory and Quarry | 645.674,000 | t Product manufactured | Contaminated land | 150202 | D9 | Yes | 1,640 | 2.089 | 0,000002539981 |
| wdt_ID | userid | Year | Center | Units | Description of the waste | CER/LER code. | Hazardous | post_author | ||||
| ∑ = 39,555,052.000 |
 |
Management of raw materials and resources |
Management of material resources
The clinker, cement and mortar manufacturing processes require the consumption of large quantities of raw materials. The main raw material used is stone extracted from the surrounding quarries, although there are also other materials that are essential in smaller quantities to achieve an adequate composition of the intermediate and final products, with external origin. For the most part, these are also natural raw materials from other operations, but circular economy principles are also applied and alternative raw materials from other industrial processes are used. Raw material consumption values depend on variations in production and consumption of alternative materials. The materials included in each category are: Natural raw materials used in clinker production: Loam , limestone, silica sand, fluorite, limonite, iron silicate, limestone sand, and limestone waste.
Secondary raw materials in clinker production: Molding sand, slag, construction and demolition waste, cement sludge and plant cleaning waste, iron scale.
Natural raw materials in cement manufacturing: Limestone, clinker, gypsum, ferrous sulfates, pozzolan, and additives.
Secondary raw materials in cement manufacturing:Flyashand blast furnace slag.
Natural raw materials in mortar production: Cement, aggregates, and lime.
Environmental management and control
In recent years, the Mataporquera plant has continued to explore options and the availability of materials to replace these natural raw materials with secondary raw materials—waste from other activities—as a means of reducing and optimizing its operations. Recovery practices Recovery a number of environmental benefits, including a reduction in the extraction of natural raw materials and the amount of waste sent to landfills, provided that they do not introduce components that affect product quality or the safety of workers and the environment.
Decarbonated raw materials have been included due to their effect on reducing CO2 emissions, such as limestone sand and limestone waste, construction and demolition waste, cement slurry, and facility cleaning waste. The use of alternative raw materials in clinker production has remained constant.
In cement production, the use of raw materials depends on the type of cement manufactured and the percentage of clinker consumed, in accordance with the UNE 197 series of standards.
In the case of mortar, raw material consumption ratios remain unchanged, and no alternative materials are used.
Evolution of specific metrics and ratios
Resource consumption
Type of materials
| wdt_ID | userid | Year | Center | Units Pr. | Units | Type of Materials | % Recycled | % Hazardous | Quantity of raw materials (t) | Quantity of Auxiliary Materials. (t) | Quantity Containers & Packs (t) | Total (t) | Total ratio (t)/LU. | Hazardous Materials (t) | Recycled Materials (t) |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| 278 | 2.089 | 2023 | Quarry | 579.797,000 | t Crushed stone | Blasting explosive | 0,000 | 100,000 | 0,000 | 44,757 | 44,76 | 0,000077 | 44,76 | 0,00 | |
| 284 | 2.089 | 2024 | Quarry | 708.600,000 | t Crushed stone | Blasting explosive | 0,000 | 100,000 | 0,000 | 41,623 | 41,62 | 0,000059 | 41,62 | 0,00 | |
| 355 | 2.089 | 2023 | Factory | 367.612,000 | t Clinker fabricated | Crushed marl | 0,000 | 0,000 | 326.041,000 | 0,000 | 0 | 326.041,00 | 0,886916 | 0,00 | 0,00 |
| 356 | 2.089 | 2023 | Factory | 367.612,000 | t Clinker fabricated | Crushed limestone | 0,000 | 0,000 | 192.466,000 | 0,000 | 0 | 192.466,00 | 0,523557 | 0,00 | 0,00 |
| 357 | 2.089 | 2023 | Factory | 367.612,000 | t Clinker fabricated | Silica sand | 0,000 | 0,000 | 27.349,000 | 0,000 | 0 | 27.349,00 | 0,074396 | 0,00 | 0,00 |
| 358 | 2.089 | 2023 | Factory | 367.612,000 | t Clinker fabricated | High alkali silica sand | 0,000 | 0,000 | 2.469,000 | 0,000 | 0 | 2.469,00 | 0,006716 | 0,00 | 0,00 |
| 359 | 2.089 | 2023 | Factory | 367.612,000 | t Clinker fabricated | Fluorite | 0,000 | 0,000 | 260,790 | 0,000 | 0 | 260,79 | 0,000709 | 0,00 | 0,00 |
| 360 | 2.089 | 2023 | Factory | 367.612,000 | t Clinker fabricated | Limonite | 0,000 | 0,000 | 1.648,000 | 0,000 | 0 | 1.648,00 | 0,004483 | 0,00 | 0,00 |
| 361 | 2.089 | 2023 | Factory | 367.612,000 | t Clinker fabricated | Ferrous silicate | 0,000 | 0,000 | 376,000 | 0,000 | 0 | 376,00 | 0,001023 | 0,00 | 0,00 |
| 362 | 2.089 | 2023 | Factory | 367.612,000 | t Clinker fabricated | Limestone sand | 0,000 | 0,000 | 7.427,000 | 0,000 | 0 | 7.427,00 | 0,020203 | 0,00 | 0,00 |
| 363 | 2.089 | 2023 | Factory | 367.612,000 | t Clinker fabricated | Limestone rejects | 0,000 | 0,000 | 4.423,000 | 0,000 | 0 | 4.423,00 | 0,012032 | 0,00 | 0,00 |
| 364 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | Crushed marl | 0,000 | 0,000 | 367.112,000 | 0,000 | 0 | 367.112,00 | 0,921531 | 0,00 | 0,00 |
| 365 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | Crushed limestone | 0,000 | 0,000 | 209.676,000 | 0,000 | 0 | 209.676,00 | 0,526332 | 0,00 | 0,00 |
| 366 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | Silica sand | 0,000 | 0,000 | 22.932,000 | 0,000 | 0 | 22.932,00 | 0,057564 | 0,00 | 0,00 |
| 367 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | High alkali silica sand | 0,000 | 0,000 | 3.361,000 | 0,000 | 0 | 3.361,00 | 0,008437 | 0,00 | 0,00 |
| 368 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | Fluorite | 0,000 | 0,000 | 100,480 | 0,000 | 0 | 100,48 | 0,000252 | 0,00 | 0,00 |
| 369 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | Limonite | 0,000 | 0,000 | 0,000 | 0,000 | 0 | 0,00 | 0,000000 | 0,00 | 0,00 |
| 370 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | Ferrous silicate | 0,000 | 0,000 | 0,000 | 0,000 | 0 | 0,00 | 0,000000 | 0,00 | 0,00 |
| 371 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | Limestone sand | 0,000 | 0,000 | 923,000 | 0,000 | 0 | 923,00 | 0,002317 | 0,00 | 0,00 |
| 372 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | Limestone rejects | 0,000 | 0,000 | 0,000 | 0,000 | 0 | 0,00 | 0,000000 | 0,00 | 0,00 |
| 379 | 2.089 | 2023 | Factory | 574.552,000 | t Cement manufactured | Plaster | 0,000 | 0,000 | 28.215,820 | 0,000 | 0 | 28.215,82 | 0,049109 | 0,00 | 0,00 |
| 380 | 2.089 | 2023 | Factory | 574.552,000 | t Cement manufactured | Limestone | 0,000 | 0,000 | 40.040,500 | 0,000 | 0 | 40.040,50 | 0,069690 | 0,00 | 0,00 |
| 381 | 2.089 | 2023 | Factory | 574.552,000 | t Cement manufactured | Clinker | 0,000 | 0,000 | 503.374,660 | 0,000 | 0 | 503.374,66 | 0,876117 | 0,00 | 0,00 |
| 382 | 2.089 | 2023 | Factory | 574.552,000 | t Cement manufactured | Ferrous sulfate | 0,000 | 0,000 | 608,080 | 0,000 | 0 | 608,08 | 0,001058 | 0,00 | 0,00 |
| 383 | 2.089 | 2023 | Factory | 574.552,000 | t Cement manufactured | Additive | 0,000 | 0,000 | 475,718 | 0,000 | 0 | 475,72 | 0,000828 | 0,00 | 0,00 |
| 384 | 2.089 | 2023 | Factory | 574.552,000 | t Cement manufactured | Pozzolana | 0,000 | 0,000 | 107,000 | 0,000 | 0 | 107,00 | 0,000186 | 0,00 | 0,00 |
| 385 | 2.089 | 2024 | Factory | 582.772,000 | t Cement manufactured | Plaster | 0,000 | 0,000 | 28.253,000 | 0,000 | 0 | 28.253,00 | 0,048480 | 0,00 | 0,00 |
| 386 | 2.089 | 2024 | Factory | 582.772,000 | t Cement manufactured | Limestone | 0,000 | 0,000 | 47.642,680 | 0,000 | 0 | 47.642,68 | 0,081752 | 0,00 | 0,00 |
| 387 | 2.089 | 2024 | Factory | 582.772,000 | t Cement manufactured | Clinker | 0,000 | 0,000 | 506.220,330 | 0,000 | 0 | 506.220,33 | 0,868642 | 0,00 | 0,00 |
| 388 | 2.089 | 2024 | Factory | 582.772,000 | t Cement manufactured | Ferrous sulfate | 0,000 | 0,000 | 48,800 | 0,000 | 0 | 48,80 | 0,000084 | 0,00 | 0,00 |
| 389 | 2.089 | 2024 | Factory | 582.772,000 | t Cement manufactured | Additive | 0,000 | 0,000 | 472,511 | 0,000 | 0 | 472,51 | 0,000811 | 0,00 | 0,00 |
| 390 | 2.089 | 2024 | Factory | 582.772,000 | t Cement manufactured | Pozzolana | 0,000 | 0,000 | 0,000 | 0,000 | 0 | 0,00 | 0,000000 | 0,00 | 0,00 |
| 394 | 2.089 | 2023 | Factory | 53.608,000 | t Manufactured mortar | Cement | 0,000 | 0,000 | 5.918,000 | 0,000 | 0 | 5.918,00 | 0,110394 | 0,00 | 0,00 |
| 395 | 2.089 | 2023 | Factory | 53.608,000 | t Manufactured mortar | Aggregates | 0,000 | 0,000 | 48.814,000 | 0,000 | 0 | 48.814,00 | 0,910573 | 0,00 | 0,00 |
| 396 | 2.089 | 2023 | Factory | 53.608,000 | t Manufactured mortar | Lime | 0,000 | 0,000 | 114,000 | 0,000 | 0 | 114,00 | 0,002127 | 0,00 | 0,00 |
| 397 | 2.089 | 2024 | Factory | 58.090,000 | t Manufactured mortar | Cement | 0,000 | 0,000 | 7.373,000 | 0,000 | 0 | 7.373,00 | 0,126924 | 0,00 | 0,00 |
| 398 | 2.089 | 2024 | Factory | 58.090,000 | t Manufactured mortar | Aggregates | 0,000 | 0,000 | 47.843,000 | 0,000 | 0 | 47.843,00 | 0,823601 | 0,00 | 0,00 |
| 399 | 2.089 | 2024 | Factory | 58.090,000 | t Manufactured mortar | Lime | 0,000 | 0,000 | 3.750,000 | 0,000 | 0 | 3.750,00 | 0,064555 | 0,00 | 0,00 |
| 407 | 2.089 | 2023 | Factory | 367.612,000 | t Clinker fabricated | Molding sand | 100,000 | 0,000 | 3.982,000 | 0,000 | 0 | 3.982,00 | 0,010832 | 0,00 | 3.982,00 |
| 408 | 2.089 | 2023 | Factory | 367.612,000 | t Clinker fabricated | Slag | 100,000 | 0,000 | 0,000 | 0,000 | 0 | 0,00 | 0,000000 | 0,00 | 0,00 |
| 409 | 2.089 | 2023 | Factory | 367.612,000 | t Clinker fabricated | RCD | 100,000 | 0,000 | 2.026,000 | 0,000 | 0 | 2.026,00 | 0,005511 | 0,00 | 2.026,00 |
| 410 | 2.089 | 2023 | Factory | 367.612,000 | t Clinker fabricated | Cement sludge | 100,000 | 0,000 | 1.400,000 | 0,000 | 0 | 1.400,00 | 0,003808 | 0,00 | 1.400,00 |
| 411 | 2.089 | 2023 | Factory | 367.612,000 | t Clinker fabricated | Recycled aggregates | 100,000 | 0,000 | 0,000 | 0,000 | 0 | 0,00 | 0,000000 | 0,00 | 0,00 |
| 412 | 2.089 | 2023 | Factory | 367.612,000 | t Clinker fabricated | Iron scale | 100,000 | 0,000 | 9.933,000 | 0,000 | 0 | 9.933,00 | 0,027020 | 0,00 | 9.933,00 |
| 413 | 2.089 | 2023 | Factory | 367.612,000 | t Clinker fabricated | Steel slag | 100,000 | 0,000 | 0,000 | 0,000 | 0 | 0,00 | 0,000000 | 0,00 | 0,00 |
| 414 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | Molding sand | 100,000 | 0,000 | 3.738,500 | 0,000 | 0 | 3.738,50 | 0,009384 | 0,00 | 3.738,50 |
| 415 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | Slag | 100,000 | 0,000 | 0,000 | 0,000 | 0 | 0,00 | 0,000000 | 0,00 | 0,00 |
| 416 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | RCD | 100,000 | 0,000 | 2.482,500 | 0,000 | 0 | 2.482,50 | 0,006232 | 0,00 | 2.482,50 |
| 417 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | Cement sludge | 100,000 | 0,000 | 2.377,480 | 0,000 | 0 | 2.377,48 | 0,005968 | 0,00 | 2.377,48 |
| 418 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | Recycled aggregates | 100,000 | 0,000 | 4.601,000 | 0,000 | 0 | 4.601,00 | 0,011550 | 0,00 | 4.601,00 |
| 419 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | Iron scale | 100,000 | 0,000 | 12.024,000 | 0,000 | 0 | 12.024,00 | 0,030183 | 0,00 | 12.024,00 |
| 420 | 2.089 | 2024 | Factory | 398.372,000 | t Clinker fabricated | Steel slag | 100,000 | 0,000 | 0,000 | 0,000 | 0 | 0,00 | 0,000000 | 0,00 | 0,00 |
| 424 | 2.089 | 2023 | Factory | 574.552,000 | t Cement manufactured | Fly ash | 100,000 | 0,000 | 1.989,000 | 0,000 | 0 | 1.989,00 | 0,003462 | 0,00 | 1.989,00 |
| 425 | 2.089 | 2023 | Factory | 574.552,000 | t Cement manufactured | Blast furnace slag | 100,000 | 0,000 | 5.003,500 | 0,000 | 0 | 5.003,50 | 0,008709 | 0,00 | 5.003,50 |
| 426 | 2.089 | 2023 | Factory | 574.552,000 | t Cement manufactured | Desulfurization gypsum | 100,000 | 0,000 | 0,000 | 0,000 | 0 | 0,00 | 0,000000 | 0,00 | 0,00 |
| 427 | 2.089 | 2024 | Factory | 582.772,000 | t Cement manufactured | Fly ash | 100,000 | 0,000 | 438,000 | 0,000 | 0 | 438,00 | 0,000752 | 0,00 | 438,00 |
| 428 | 2.089 | 2024 | Factory | 582.772,000 | t Cement manufactured | Blast furnace slag | 100,000 | 0,000 | 4.918,000 | 0,000 | 0 | 4.918,00 | 0,008439 | 0,00 | 4.918,00 |
| 429 | 2.089 | 2024 | Factory | 582.772,000 | t Cement manufactured | Desulfurization gypsum | 100,000 | 0,000 | 0,000 | 0,000 | 0 | 0,00 | 0,000000 | 0,00 | 0,00 |
| 693 | 2.089 | 2025 | Factory | 433.549,000 | t Clinker fabricated | Molding sand | 100,000 | 0,000 | 4.803,000 | 0,000 | 0 | 4.803,00 | 0,011078 | 0,00 | 4.803,00 |
| 694 | 2.089 | 2025 | Factory | 433.549,000 | t Clinker fabricated | Slag | 100,000 | 0,000 | 0,000 | 0,000 | 0 | 0,00 | 0,000000 | 0,00 | 0,00 |
| 695 | 2.089 | 2025 | Factory | 433.549,000 | t Clinker fabricated | RCD | 100,000 | 0,000 | 7.279,140 | 0,000 | 0 | 7.279,14 | 0,016790 | 0,00 | 7.279,14 |
| 696 | 2.089 | 2025 | Factory | 433.549,000 | t Clinker fabricated | Cement sludge | 100,000 | 0,000 | 1.526,840 | 0,000 | 0 | 1.526,84 | 0,003522 | 0,00 | 1.526,84 |
| 697 | 2.089 | 2025 | Factory | 433.549,000 | t Clinker fabricated | Recycled aggregates | 100,000 | 0,000 | 0,000 | 0,000 | 0 | 0,00 | 0,000000 | 0,00 | 0,00 |
| 698 | 2.089 | 2025 | Factory | 433.549,000 | t Clinker fabricated | Iron scale | 100,000 | 0,000 | 14.663,000 | 0,000 | 0 | 14.663,00 | 0,033821 | 0,00 | 14.663,00 |
| 699 | 2.089 | 2025 | Factory | 433.549,000 | t Clinker fabricated | Decarbonated sludge (landfill) | 100,000 | 0,000 | 1.067,460 | 0,000 | 0 | 1.067,46 | 0,002462 | 0,00 | 1.067,46 |
| 701 | 2.089 | 2025 | Factory | 581.843,000 | t Cement manufactured | Fly ash | 100,000 | 0,000 | 1.245,000 | 0,000 | 0 | 1.245,00 | 0,002140 | 0,00 | 1.245,00 |
| 702 | 2.089 | 2025 | Factory | 581.843,000 | t Cement manufactured | Blast furnace slag | 100,000 | 0,000 | 4.901,000 | 0,000 | 0 | 4.901,00 | 0,008423 | 0,00 | 4.901,00 |
| 703 | 2.089 | 2025 | Factory | 581.843,000 | t Cement manufactured | Desulfurization gypsum | 100,000 | 0,000 | 0,000 | 0,000 | 0 | 0,00 | 0,000000 | 0,00 | 0,00 |
| 757 | 2.089 | 2025 | Factory | 433.549,000 | t Clinker fabricated | Crushed marl | 0,000 | 0,000 | 384.685,056 | 0,000 | 0 | 384.685,06 | 0,887293 | 0,00 | 0,00 |
| 758 | 2.089 | 2025 | Factory | 433.549,000 | t Clinker fabricated | Crushed limestone | 0,000 | 0,000 | 231.730,000 | 0,000 | 0 | 231.730,00 | 0,534496 | 0,00 | 0,00 |
| 759 | 2.089 | 2025 | Factory | 433.549,000 | t Clinker fabricated | Silica sand | 0,000 | 0,000 | 20.956,500 | 0,000 | 0 | 20.956,50 | 0,048337 | 0,00 | 0,00 |
| 760 | 2.089 | 2025 | Factory | 433.549,000 | t Clinker fabricated | High alkali silica sand | 0,000 | 0,000 | 6.361,000 | 0,000 | 0 | 6.361,00 | 0,014672 | 0,00 | 0,00 |
| 762 | 2.089 | 2025 | Factory | 433.549,000 | t Clinker fabricated | Limestone sand | 0,000 | 0,000 | 1.800,004 | 0,000 | 0 | 1.800,00 | 0,004152 | 0,00 | 0,00 |
| 933 | 2.089 | 2025 | Factory | 582.843,000 | t Cement manufactured | Plaster | 0,000 | 0,000 | 28.369,600 | 0,000 | 0 | 28.369,60 | 0,048675 | 0,00 | 0,00 |
| 934 | 2.089 | 2025 | Factory | 581.843,000 | t Cement manufactured | Limestone | 0,000 | 0,000 | 50.305,710 | 0,000 | 0 | 50.305,71 | 0,086459 | 0,00 | 0,00 |
| 935 | 2.089 | 2025 | Factory | 581.843,000 | t Cement manufactured | Clinker | 0,000 | 0,000 | 501.763,980 | 0,000 | 0 | 501.763,98 | 0,862370 | 0,00 | 0,00 |
| 936 | 2.089 | 2025 | Factory | 581.843,000 | t Cement manufactured | Ferrous sulfate | 0,000 | 0,000 | 77,700 | 0,000 | 0 | 77,70 | 0,000134 | 0,00 | 0,00 |
| 937 | 2.089 | 2025 | Factory | 581,843 | t Cement manufactured | Additive | 0,000 | 0,000 | 387,730 | 0,000 | 0 | 387,73 | 0,666383 | 0,00 | 0,00 |
| 938 | 2.089 | 2025 | Quarry | 663.668,000 | t Crushed stone | Blasting explosive | 0,000 | 100,000 | 0,000 | 38,675 | 38,68 | 0,000058 | 38,68 | 0,00 | |
| wdt_ID | Year | Center | Units | Type of Materials | |||||||||||
| ∑ = 34,235,889.843 |
Relevant aggregated data
| wdt_ID | userid | Year | Center | Units Pr. | Units | Type of Materials | % Recycled | % Hazardous | Quantity of raw materials (t) | Quantity of Auxiliary Materials. (t) | Quantity Containers & Packs (t) | Total (t) | Total ratio (t)/LU. | Hazardous Materials (t) | Recycled Materials (t) |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| wdt_ID | Year | Center | Type of Materials | ||||||||||||
| ∑ = |
 |
Biodiversity |
Biodiversity indicators
The manufacturing facilities occupy a built-up area of 39,507 m2 , which includes the mortar plant with a built-up area of 1,678m2 . The adjacent quarry occupies a constructed area of 2,883m2 and an operating area of 777,200m2. The main impact of our activity on the landscape is the exploitation of natural resources in the raw material supply quarry, and the Group has defined as a future challenge the "development of integrated management criteria for the restoration of quarries and the promotion of biodiversity". The area currently restored is 11,050m2, and actions are established annually to comply with the restoration requirements included in the Work Plan. In 2025, no restoration work was carried out because there were no available areas due to the quarry’s operating system, which expands the working faces in a radial pattern to continue mining downward once the boundary surrounding the entire quarry is reached. Vertical mining is limited by the water table.
| wdt_ID | userid | post_author | Year | Center | Units Pr. | Units | Total land use (m2) | Sealed surface area (m²) | Unsealed area (m2) | Land use / nature | Area oriented according to nature at the site (m²) | Non-central area oriented according to nature (m²) | Usage ratio (m2)/Udp. | Sealed ratio (m2)/Udp. | Unsealed Ratio (m2/Udp) | Targeted ratio (m2)/Udp. | Off-center ratio (m2)/Udp. |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| 108 | 2.089 | 2.089 | 2023 | Factory | 628.160,000 | t Product manufactured | 39.507 | 39.507 | -39.507 | 39.507 | 0 | 0,0000 | 0,0000 | 0,0000 | 0,0000 | 0,0000 | |
| 109 | 2.089 | 2.089 | 2024 | Factory | 640.862,000 | t Product manufactured | 39.687 | 39.687 | -39.507 | 39.507 | 0 | 0,0000 | 0,0000 | 0,0000 | 0,0000 | 0,0000 | |
| 110 | 2.089 | 2.089 | 2024 | Quarry | 708.600,000 | Production/Service Unit | 947.525 | 2.883 | 944.642 | 506.957 | 0 | 0,0000 | 0,0000 | 0,0000 | 0,0000 | 0,0000 | |
| 183 | 2.089 | 2.089 | 2025 | Factory | 645.674,000 | t Product manufactured | 39.687 | 39.687 | -39.507 | 39.507 | 0 | 0,0000 | 0,0000 | 0,0000 | 0,0000 | 0,0000 | |
| 184 | 2.089 | 2.089 | 2025 | Quarry | 663.668,000 | Production/Service Unit | 947.525 | 2.883 | 944.642 | 506.957 | 0 | 0,0000 | 0,0000 | 0,0000 | 0,0000 | 0,0000 | |
| Year | Center | ||||||||||||||||
| ∑ = 3,286,964.000 |
 |
Other information of environmental interest |
Indicators and impacts
In 2026, it is important to highlight the environmental impact of the fire at the storage and Recovery facility Recovery solid alternative fuels serving the main burner. The fire generated wood, scrap metal, and inert material in quantities exceeding those of normal operations. It also resulted in emissions and wastewater discharges typical of an emergency and firefighting situation, and an increase in the consumption of captured water was observed. The fire has also led to a shift away from biomass fuels toward fossil fuels. The factory’s greenhouse gas emissions trajectory for 2025 was on track to achieve an emissions factor of less than 722 kg of CO2 per ton of clinker, which would have meant that the facility would meet the criteria of the European Taxonomy to be considered aligned with climate change mitigation. Following the fire, a plan is being implemented to improve the fire prevention and suppression system, along with a comprehensive review of the Self-Protection Plan.
Significant and/or sector specific indicators
Sound emissions
Noise emissions in the surroundings of the manufacturing facilities generate, as an impact, nuisances to the population and fauna. In the case of the Mataporquera factory, located in the center of the municipality and very close to residential dwellings, a series of actions have been undertaken to minimize this impact and achieve noise emission levels below the established VLE.
A measurement campaign is conducted annually at representative locations on the outskirts of the city to ensure compliance with the legal requirements established for the factory. All measured values are below the limit values, both during the day and at night.
| wdt_ID | userid | Year | Center | Units | Units Pr. | Indicator description | Origin / Type / Appearance | Value | Unit of value | Information | post_author | Pr. Ratio |
|---|---|---|---|---|---|---|---|---|---|---|---|---|
| 249 | 2.089 | 2023 | Factory | t Product manufactured | 628.160,000 | Point 1 in front of the first aid kit | Noise Emissions Factory Measurement DAY | 57,100 | Decibels (dBA) | 2.089 | 0,000000 | |
| 250 | 2.089 | 2023 | Factory | t Product manufactured | 628.160,000 | Point 2 in front of substation | Noise Emissions Factory Measurement DAY | 54,600 | Decibels (dBA) | 2.089 | 0,000000 | |
| 251 | 2.089 | 2023 | Factory | t Product manufactured | 628.160,000 | Point 3 in front of maintenance offices | Noise Emissions Factory Measurement DAY | 55,600 | Decibels (dBA) | 2.089 | 0,000000 | |
| 252 | 2.089 | 2023 | Factory | t Product manufactured | 628.160,000 | Point 4 in front of the packaging plant | Noise Emissions Factory Measurement DAY | 59,600 | Decibels (dBA) | 2.089 | 0,000000 | |
| 253 | 2.089 | 2023 | Factory | t Product manufactured | 628.160,000 | Point 5 in front of the factory entrance | Noise Emissions Factory Measurement DAY | 58,600 | Decibels (dBA) | 2.089 | 0,000000 | |
| 254 | 2.089 | 2023 | Factory | t Product manufactured | 628.160,000 | Item 6 clinker and cement silos | Noise Emissions Factory Measurement DAY | 57,700 | Decibels (dBA) | 2.089 | 0,000000 | |
| 255 | 2.089 | 2023 | Factory | t Product manufactured | 628.160,000 | Point 7 entrance to polygon P-20 | Noise Emissions Factory Measurement DAY | 57,400 | Decibels (dBA) | 2.089 | 0,000000 | |
| 256 | 2.089 | 2023 | Factory | t Product manufactured | 628.160,000 | Point 8 nearest highway exit | Noise Emissions Factory Measurement DAY | 50,300 | Decibels (dBA) | 2.089 | 0,000000 | |
| 266 | 2.089 | 2023 | Factory | t Product manufactured | 628.160,000 | Point 1 in front of the first aid kit | Noise Emissions Factory Measurement NIGHT | 55,600 | Decibels (dBA) | 2.089 | 0,000000 | |
| 267 | 2.089 | 2023 | Factory | t Product manufactured | 628.160,000 | Point 2 in front of substation | Noise Emissions Factory Measurement NIGHT | 58,600 | Decibels (dBA) | 2.089 | 0,000000 | |
| 268 | 2.089 | 2023 | Factory | t Product manufactured | 628.160,000 | Point 3 in front of maintenance offices | Noise Emissions Factory Measurement NIGHT | 59,400 | Decibels (dBA) | 2.089 | 0,000000 | |
| 269 | 2.089 | 2023 | Factory | t Product manufactured | 628.160,000 | Point 4 in front of the packaging plant | Noise Emissions Factory Measurement NIGHT | 60,500 | Decibels (dBA) | 2.089 | 0,000000 | |
| 270 | 2.089 | 2023 | Factory | t Product manufactured | 628.160,000 | Point 5 in front of the factory entrance | Noise Emissions Factory Measurement NIGHT | 59,200 | Decibels (dBA) | 2.089 | 0,000000 | |
| 271 | 2.089 | 2023 | Factory | t Product manufactured | 628.160,000 | Item 6 clinker and cement silos | Noise Emissions Factory Measurement NIGHT | 59,200 | Decibels (dBA) | 2.089 | 0,000000 | |
| 272 | 2.089 | 2023 | Factory | t Product manufactured | 628.160,000 | Point 7 entrance to polygon P-20 | Noise Emissions Factory Measurement NIGHT | 60,800 | Decibels (dBA) | 2.089 | 0,000000 | |
| 273 | 2.089 | 2023 | Factory | t Product manufactured | 628.160,000 | Point 8 nearest highway exit | Noise Emissions Factory Measurement NIGHT | 46,400 | Decibels (dBA) | 2.089 | 0,000000 | |
| 284 | 2.089 | 2024 | Factory | t Product manufactured | 640.862,000 | Point 1 in front of the first aid kit | Noise Emissions Factory Measurement DAY | 50,900 | Decibels (dBA) | 2.089 | 0,000000 | |
| 285 | 2.089 | 2024 | Factory | t Product manufactured | 640.862,000 | Point 2 in front of substation | Noise Emissions Factory Measurement DAY | 54,700 | Decibels (dBA) | 2.089 | 0,000000 | |
| 286 | 2.089 | 2024 | Factory | t Product manufactured | 640.862,000 | Point 3 in front of maintenance offices | Noise Emissions Factory Measurement DAY | 56,400 | Decibels (dBA) | 2.089 | 0,000000 | |
| 287 | 2.089 | 2024 | Factory | t Product manufactured | 640.862,000 | Point 4 in front of the packaging plant | Noise Emissions Factory Measurement DAY | 58,700 | Decibels (dBA) | 2.089 | 0,000000 | |
| 288 | 2.089 | 2024 | Factory | t Product manufactured | 640.862,000 | Point 5 in front of the factory entrance | Noise Emissions Factory Measurement DAY | 60,800 | Decibels (dBA) | 2.089 | 0,000000 | |
| 289 | 2.089 | 2024 | Factory | t Product manufactured | 640.862,000 | Item 6 clinker and cement silos | Noise Emissions Factory Measurement DAY | 59,200 | Decibels (dBA) | 2.089 | 0,000000 | |
| 290 | 2.089 | 2024 | Factory | t Product manufactured | 640.862,000 | Point 7 entrance to polygon P-20 | Noise Emissions Factory Measurement DAY | 58,800 | Decibels (dBA) | 2.089 | 0,000000 | |
| 291 | 2.089 | 2024 | Factory | t Product manufactured | 640.862,000 | Point 8 nearest highway exit | Noise Emissions Factory Measurement DAY | 45,800 | Decibels (dBA) | 2.089 | 0,000000 | |
| 292 | 2.089 | 2024 | Factory | t Product manufactured | 640.862,000 | Point 1 in front of the first aid kit | Noise Emissions Factory Measurement NIGHT | 50,700 | Decibels (dBA) | 2.089 | 0,000000 | |
| 293 | 2.089 | 2024 | Factory | t Product manufactured | 640.862,000 | Point 2 in front of substation | Noise Emissions Factory Measurement NIGHT | 54,500 | Decibels (dBA) | 2.089 | 0,000000 | |
| 294 | 2.089 | 2024 | Factory | t Product manufactured | 640.862,000 | Point 3 in front of maintenance offices | Noise Emissions Factory Measurement NIGHT | 55,800 | Decibels (dBA) | 2.089 | 0,000000 | |
| 295 | 2.089 | 2024 | Factory | t Product manufactured | 640.862,000 | Point 4 in front of the packaging plant | Noise Emissions Factory Measurement NIGHT | 57,300 | Decibels (dBA) | 2.089 | 0,000000 | |
| 296 | 2.089 | 2024 | Factory | t Product manufactured | 640.862,000 | Point 5 in front of the factory entrance | Noise Emissions Factory Measurement NIGHT | 60,300 | Decibels (dBA) | 2.089 | 0,000000 | |
| 297 | 2.089 | 2024 | Factory | t Product manufactured | 640.862,000 | Item 6 clinker and cement silos | Noise Emissions Factory Measurement NIGHT | 57,800 | Decibels (dBA) | 2.089 | 0,000000 | |
| 298 | 2.089 | 2024 | Factory | t Product manufactured | 640.862,000 | Point 7 entrance to polygon P-20 | Noise Emissions Factory Measurement NIGHT | 56,800 | Decibels (dBA) | 2.089 | 0,000000 | |
| 299 | 2.089 | 2024 | Factory | t Product manufactured | 640.862,000 | Point 8 nearest highway exit | Noise Emissions Factory Measurement NIGHT | 45,700 | Decibels (dBA) | 2.089 | 0,000000 | |
| 482 | 2.089 | 2025 | Factory | t Product manufactured | 645.674,000 | Point 1 in front of the first aid kit | Noise Emissions Factory Measurement DAY | 51,200 | Decibels (dBA) | 2.089 | 0,000000 | |
| 483 | 2.089 | 2025 | Factory | t Product manufactured | 645.674,000 | Point 2 in front of substation | Noise Emissions Factory Measurement DAY | 55,200 | Decibels (dBA) | 2.089 | 0,000000 | |
| 484 | 2.089 | 2025 | Factory | t Product manufactured | 645.674,000 | Point 3 in front of maintenance offices | Noise Emissions Factory Measurement DAY | 58,500 | Decibels (dBA) | 2.089 | 0,000000 | |
| 485 | 2.089 | 2025 | Factory | t Product manufactured | 645.674,000 | Point 4 in front of the packaging plant | Noise Emissions Factory Measurement DAY | 59,100 | Decibels (dBA) | 2.089 | 0,000000 | |
| 486 | 2.089 | 2025 | Factory | t Product manufactured | 645.674,000 | Point 5 in front of the factory entrance | Noise Emissions Factory Measurement DAY | 61,100 | Decibels (dBA) | 2.089 | 0,000000 | |
| 487 | 2.089 | 2025 | Factory | t Product manufactured | 645.674,000 | Item 6 clinker and cement silos | Noise Emissions Factory Measurement DAY | 60,000 | Decibels (dBA) | 2.089 | 0,000000 | |
| 488 | 2.089 | 2025 | Factory | t Product manufactured | 645.674,000 | Point 7 entrance to polygon P-20 | Noise Emissions Factory Measurement DAY | 57,900 | Decibels (dBA) | 2.089 | 0,000000 | |
| 489 | 2.089 | 2025 | Factory | t Product manufactured | 645.674,000 | Point 8 nearest highway exit | Noise Emissions Factory Measurement DAY | 45,400 | Decibels (dBA) | 2.089 | 0,000000 | |
| 490 | 2.089 | 2025 | Factory | t Product manufactured | 645.674,000 | Point 1 in front of the first aid kit | Noise Emissions Factory Measurement NIGHT | 51,300 | Decibels (dBA) | 2.089 | 0,000000 | |
| 491 | 2.089 | 2025 | Factory | t Product manufactured | 645.674,000 | Point 2 in front of substation | Noise Emissions Factory Measurement NIGHT | 54,900 | Decibels (dBA) | 2.089 | 0,000000 | |
| 492 | 2.089 | 2025 | Factory | t Product manufactured | 645.674,000 | Point 3 in front of maintenance offices | Noise Emissions Factory Measurement NIGHT | 58,600 | Decibels (dBA) | 2.089 | 0,000000 | |
| 493 | 2.089 | 2025 | Factory | t Product manufactured | 645.674,000 | Point 4 in front of the packaging plant | Noise Emissions Factory Measurement NIGHT | 59,100 | Decibels (dBA) | 2.089 | 0,000000 | |
| 494 | 2.089 | 2025 | Factory | t Product manufactured | 645.674,000 | Point 5 in front of the factory entrance | Noise Emissions Factory Measurement NIGHT | 60,900 | Decibels (dBA) | 2.089 | 0,000000 | |
| 495 | 2.089 | 2025 | Factory | t Product manufactured | 645.674,000 | Item 6 clinker and cement silos | Noise Emissions Factory Measurement NIGHT | 59,700 | Decibels (dBA) | 2.089 | 0,000000 | |
| 496 | 2.089 | 2025 | Factory | t Product manufactured | 645.674,000 | Point 7 entrance to polygon P-20 | Noise Emissions Factory Measurement NIGHT | 57,600 | Decibels (dBA) | 2.089 | 0,000000 | |
| 497 | 2.089 | 2025 | Factory | t Product manufactured | 645.674,000 | Point 8 nearest highway exit | Noise Emissions Factory Measurement NIGHT | 44,900 | Decibels (dBA) | 2.089 | 0,000000 | |
| wdt_ID | userid | Year | Center | Units | Origin / Type / Appearance | post_author | ||||||
| ∑ = 30,635,136.00 |
Map of environmental noise immission control points.
Noise emission controls correspond to official controls performed by an Accredited Control Body.

 |
Environmental aspects and impacts |
Environmental aspects and impacts
The identification of environmental aspects is based on an analysis of the processes, facilities and products of the factory and quarry with a life cycle approach of the manufactured products. This identification, objective and quantitative, takes into account possible interactions with the environment - soil, water, atmosphere, natural environment, socio-economic environment, population, etc. - as well as normal and abnormal operating and functioning conditions, potential accidental or emergency situations, indirectly generated aspects and those that may derive from past activities, aware of the importance of adopting preventive measures at the source of our actions.

Description of the most important and significant environmental aspects
The evaluation of environmental aspects is a starting point for the revision of the System and for the definition and updating of operational control procedures, and those for action in the event of potential accidents and emergency situations. The evaluation carried out annually on environmental aspects, in general, is established on the basis of a series of definitive environmental criteria as indicated.
- Hazard or level of environmental impact of the aspect.
- Quantity or volume of the environmental aspect.
- Complaints received from stakeholders and legal non-compliance.
- Severity or level of severity of the impact, generally associated with the intrinsic and objective hazard.
- Probability, frequency or recurrence with which the aspect occurs.
- Capacity to influence economic, technical or human resources to carry out actions for prevention, control and correction of the aspect.
Based on the evaluation carried out, the significant environmental aspects with the greatest impact are determined and which, therefore, have a score higher than that established as significant, in accordance with the criteria indicated. Based on these, the activity plans its operational control and improvement objectives.
Direct environmental aspects are those generated as a result of the activities of the factory and quarry over which there is full control of their management. Grouped according to their environmental vector, the following environmental aspects have been identified and evaluated under normal and abnormal conditions.
Indirect environmental aspects are those aspects derived from the factory's activities, products and services over which there is no full control of their management. The following have been identified and evaluated as environmental aspects to be taken into account:
- Greenhouse gas emissions as a result of the transportation of purchased products.
- Greenhouse gas emissions from electricity consumption.
- Packaging waste placed on the market once it has been used.
The assessment is based on the following environmental criteria: quantity—compared to the previous year—and potential for impact—based on the possibility of implementing measures to reduce them. A comparison of environmental management data from 2025 with that from 2024 has identified emissions, discharges, and waste generated by the fire, as well as water consumption, as significant factors.
To minimize the risk of fire, the Self-Protection Plan is being reviewed, and improvements are being made to the fire prevention and control system.
Goals have also been set to minimize the water footprint and reduce leaks in older drinking water service lines.
Description of significant environmental aspects
| wdt_ID | state | userid | Year | Center | Life Cycle Phase | Environmental Aspect | Impact | Typology | Process | udimpact | Actions | Analysis | Significant | ID | post_author |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| 1.195 | VALIDATED | 2.089 | 2024 | Factory | PRODUCTION | PST | AIR POLLUTION | Direct | ATMOSPHERIC EMISSIONS IN FURNACES (ALTERNATIVE FUEL) | 15 | Yes | 138.963 | 2.089 | ||
| 1.196 | VALIDATED | 2.089 | 2024 | Factory | PRODUCTION | PST chiller | AIR POLLUTION | Direct | ATMOSPHERIC EMISSIONS AT OTHER SOURCES | 10 | Yes | 138.963 | 2.089 | ||
| 1.197 | VALIDATED | 2.089 | 2024 | Factory | PRODUCTION | MES Item 5 | WATER DISTURBANCE | Direct | WASTEWATER DISCHARGES | 15 | Yes | 138.963 | 2.089 | ||
| 1.473 | VALIDATED | 2.089 | 2025 | Factory | PRODUCTION | Water consumption | RESOURCE DEPLETION | Direct | Factory and quarry operations | 15 | Plan to improve the fire prevention and suppression system. Operational measures to enhance leak control and reduce consumption of drinking water and collected water. A water footprint target is established. | Yes | 138.963 | 2.089 | |
| 1.474 | VALIDATED | 2.089 | 2025 | Factory | PRODUCTION | Emissions from abnormal conditions | AIR POLLUTION | Direct | Production | Plan for Improving the Fire Prevention and Suppression System | Fire in September 2025 | Yes | 138.963 | 2.089 | |
| 1.478 | VALIDATED | 2.089 | 2025 | Factory | PRODUCTION | Generation of scrap metal and waste sent to landfills | GENERATION OF Hazardous WASTE | Direct | Production | Plan for Improving the Fire Prevention and Suppression System | Yes | 138.963 | 2.089 | ||
| 1.479 | VALIDATED | 2.089 | 2025 | Factory | PRODUCTION | Production of refractory bricks | GENERATION OF Hazardous WASTE | Direct | Production | We still need to remove 30 tons in 2026 to clear out obsolete material from the warehouse. | Removal of obsolete inventory from the warehouse | Yes | 138.963 | 2.089 | |
| 1.480 | VALIDATED | 2.089 | 2025 | Factory | PRODUCTION | Generation of paper waste | GENERATION OF Hazardous WASTE | Direct | Production | Disposal of obsolete paper bags | Yes | 138.963 | 2.089 | ||
 |
Environmental improvement planning |
Target Planning
The environmental program is the tool for minimizing environmental impacts as far as possible, starting with the significant ones. It is prepared based on the basic principles established in the Environmental Policy and is updated annually. For planning purposes, we take into account the results of the evaluation of aspects, risks and opportunities, legal requirements, non-conformities and incidents, the opinion of interested parties and technological options for implementing improvement opportunities. The modernization and continuous improvement of our production facilities are the basis for the reduction of the environmental aspects of our process, through the implementation of the best available techniques for the prevention, control and minimization of pollution. In 2025, the following investments were made to minimize environmental and energy-related risks:
Environmental improvement planning
This table shows the results of the Environmental Program’s achievement of its objectives and targets for the year 2025. Progress toward these goals has been monitored through meetings of the plant-level Environmental Committees and the Environmental Committees of the Spain Business Division, which operate at the corporate level.
The following are the planned improvement objectives (2023 - 2025)
| userid | wdt_ID | Year | Center | Life Cycle Phase | Objective | Goal / Action | Impact/Associated Impact | Target Value | Value reached | % Achieved | Department / Resource | Deadline | Remarks | post_author |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| 2.089 | 394 | 2025 | Factory | PRODUCTION | 1. Achieve a thermal substitution percentage of 70% through the use of alternative fuels. Consolidated by 2025. | 70 % cumulative annual thermal replacement | Depletion of natural resources | 70,000 | 60,100 | 85,9 | Environment | 31/12/2025 | Target not met due to a fire at the storage and metering facility for solid alternatives to the main burner | 2.089 |
| 2.089 | 395 | 2025 | Factory | PRODUCTION | 2. Achieve a thermal substitution percentage of 30% through the use of alternative biomass fuels. Consolidated by 2025. | 30 % cumulative annual biomass thermal substitution | Depletion of natural resources | 30,000 | 25,400 | 84,7 | Environment | 31/12/2025 | Target not met due to a fire at the storage and metering facility for solid alternatives to the main burner | 2.089 |
| 2.089 | 396 | 2025 | Factory | PRODUCTION | 3. Reach a material substitution percentage in the manufacture of crude oil of 7%. Consolidated in 2025. | 7 % cumulative annual material replacement | Depletion of natural resources | 7,000 | 10,000 | 142,9 | Environment | 31/12/2025 | Goal achieved | 2.089 |
| 2.089 | 397 | 2025 | Factory | PRODUCTION | 4. Reach a material substitution percentage with partially decarbonated materials in the manufacture of crude oil of 2%. Consolidated by 2025. | 2 % substitution of decarbonated materials per year accumulated | Depletion of natural resources | 2,000 | 5,500 | 275,0 | Environment | 31/12/2025 | Goal achieved | 2.089 |
| 2.089 | 398 | 2025 | Factory | PRODUCTION | 5. Decrease in CO2 emissions below 0.725 t of CO2 / t of clinker. Consolidated in 2025. | 0.725 t of CO2 / t of clinker | CO2 emissions | 0,722 | 0,724 | 99,2 | Environment | 31/12/2025 | Target not met due to a fire at the storage and metering facility for solid alternatives to the main burner | 2.089 |
| 2.089 | 399 | 2025 | Factory | PRODUCTION | 6. Reduction of electricity consumption below 133 kwh/t cement. Consolidated in 2025. | 133 kwh/t cement | Depletion of natural resources | 133,000 | 119,000 | 111,8 | Environment | 31/12/2025 | Goal achieved | 2.089 |
| 2.089 | 400 | 2025 | Factory | PRODUCTION | 7. Decrease the average electricity consumption of the crude oil mill for the years 2022 to 2025 below the average for the years 2020 to 2024: 16.93 KWh/t crude oil. | 16.93 kwh/t crude meal produced | Depletion of natural resources | 16,930 | 16,730 | 101,2 | Environment | 31/12/2025 | Goal achieved | 2.089 |
| 2.089 | 401 | 2025 | Factory | PRODUCTION | 8. Decrease the average electricity consumption of the cement mill for the years 2022 to 2025 below the average for the years 2020 to 2024: 48.42 KWh/t Cement. | 48.42kwh/t cement manufactured | Depletion of natural resources | 48,420 | 45,800 | 105,7 | Environment | 31/12/2025 | Goal achieved | 2.089 |
| 2.089 | 402 | 2025 | Factory | PRODUCTION | 9. Reducción del consumo térmico del horno < 3.700 MJ/t clinker. Consolidado en 2025. | 3,700 MJ/ton of clinker | Depletion of natural resources | 3.700,000 | 3.437,000 | 107,7 | Environment | 31/12/2025 | Goal achieved | 2.089 |
| 2.089 | 403 | 2025 | Factory | PRODUCTION | 10. Decrease general dust emissions to the outside. | "0" Dust emission complaints | Atmospheric emissions | 0,000 | 0,000 | 100,0 | Environment | 31/12/2025 | Goal achieved | 2.089 |
| 2.089 | 541 | 2026 | Factory | PRODUCTION | 1. Cumulative annual thermal replacement rate > 65% | 1.1. Consumption of alternative fuels. Main burner and precalcination installation: 20,000 t of fuel blending, 2,000 t of CDR, 17,000 t of flour, 2,000 t of olive pomace, 20,000 t of tires. 1.2. Furnace Expert System 1.3. Polisyus Report Measures 1.4. Hypatia Report |
Depletion of natural resources | 65,000 | 0,000 | 0,0 | Environmental Manager / Production Manager / Electrical Maintenance Manager / Quarry Manager | December 31, 2027 | 1.1 Expected deadline: Dec. 26 1.2 Expected deadline: Dec. 27 1.3 Expected deadline: Dec. 26 1.4 Expected deadline: Dec. 26 |
2.089 |
| 2.089 | 542 | 2026 | Factory | PRODUCTION | 2. Cumulative annual biomass thermal substitution rate > 26% | 2.1. Alternative Fuel Consumption Main Burner and Precalcination Unit: 17,000 tons of flour, 2,000 tons of olive pomace, 20,000 tons of tires, and 2,000 tons of CDR. 2.2. Furnace Expert System 2.3. Polisyus Report Measures 2.4. Hypatia Report |
Depletion of natural resources | 26,000 | 0,000 | 0,0 | Environmental Manager / Production Manager / Electrical Maintenance Manager / Quarry Manager | December 31, 2027 | 2.1 Expected deadline: Dec. 26 2.2 Expected deadline: Dec. 27 2.3 Expected deadline: Dec. 26 2.4 Expected deadline: Dec. 26 |
2.089 |
| 2.089 | 543 | 2026 | Factory | PRODUCTION | 3. Annual material substitution rate relative to cumulative crude oil production > 5% | 3.1 Use of available alternative raw materials: 5,000 tons of rice husks and iron, 2,500 tons of facility cleanup waste, 1,000 tons of construction and demolition waste, 2,000 tons of cement sludge, 6,000 tons of sand from mold removal. 3.2 Search for new sources and suitable alternative raw materials. |
Depletion of natural resources | 5,000 | 0,000 | 0,0 | Environmental Manager / Production Manager | December 31, 2026 | 3.1 Expected deadline: Dec. 2026 3.2 Expected deadline: Dec. 2026 |
2.089 |
| 2.089 | 544 | 2026 | Factory | PRODUCTION | 4. Annual percentage of decarbonized materials used in place of crude oil, relative to cumulative crude oil usage, is greater than 2% | 4.1 Use of available alternative raw materials: 2,500 tons of facility cleanup waste, 1,000 tons of construction and demolition waste (CDW), 2,000 tons of cement slurry, and 30,000 tons of limestone waste. 4.2 Search for new sources and suitable decarbonated raw materials. |
Depletion of natural resources | 2,000 | 0,000 | 0,0 | Environmental Manager / Production Manager | December 31, 2026 | 4.1 Expected deadline: Dec. 2026 4.2 Expected deadline: Dec. 2026 |
2.089 |
| 2.089 | 545 | 2026 | Factory | PRODUCTION | 5. Cumulative annual replacement rate of decarbonated materials > 2% | 5.1 Meeting the targets for Recovery of biomass 5.2 Meeting the target Recovery decarbonized Recovery 5.3 Meeting the targets for thermal efficiency |
Climate change | 0,722 | 0,000 | 0,0 | Environmental Manager / Production Manager | December 31, 2026 | 5.1 Expected deadline: Dec. 26 5.2 Expected deadline: Dec. 26 5.3 Expected deadline: Dec. 26 |
2.089 |
| 2.089 | 546 | 2026 | Factory | PRODUCTION | 6. Average energy consumption (kWh/t) of the cement mill for the years 2024 to 2026: 47.64 kWh/t of cement produced | 6.1 Renovation of the mill feed system 6.2 Optimization of the Expert System for Cement Mill Operation |
Climate change | 47,640 | 0,000 | 0,0 | Head of Mechanical Maintenance / Production Manager | December 31, 2026 | 6.1 Expected deadline: Jan. 2026 6.2 Expected deadline: Dec. 2026 |
2.089 |
| 2.089 | 547 | 2026 | Factory | PRODUCTION | 7. Average energy consumption (kWh/t) of the raw meal mill from 2024 to 2026: 16.92 kWh/t of raw meal produced | 7.1 Replacement of raw mill liners. 7.2 Optimization of the Expert Control System for the Quadropol Mill |
Consumption of natural resources | 16,920 | 0,000 | 0,0 | Head of Mechanical Maintenance / Head of Manufacturing / Head of Electrical Maintenance | December 31, 2026 | 7.1 Expected deadline: Dec. 20 7.2 Expected deadline: Dec. 20 |
2.089 |
| 2.089 | 548 | 2026 | Factory | PRODUCTION | 8. Consumo específico de energía térmica < 3430 kcal/tclinker | 8.1 Optimization of expert control systems for the kiln. 8.2 Minimizing false air intake. 8.3 Optimizing process control using kiln quality control data. 8.4 Retrofit of the calciner and tertiary air ducts. |
Consumption of natural resources | 3.430,000 | 0,000 | 0,0 | Head of Mechanical Maintenance / Head of Manufacturing / Head of Electrical Maintenance / Head of Production. | December 31, 2027 | 8.1 Expected deadline: Dec. 27 8.2 Expected deadline: Dec. 26 8.2 Expected deadline: Dec. 26 8.2 Expected deadline: Dec. 26 |
2.089 |
| 2.089 | 549 | 2026 | Factory | PRODUCTION | 9. Zero complaints regarding dust emissions | 9.1 Quarry irrigation during the summer months. 9.2 Monitoring of filters and sources of process dust. |
Air Pollution | 0,000 | 0,000 | 0,0 | Production Manager / Quarry | December 31, 2026 | 9.1 Expected deadline: Dec. 2026 9.2 Expected deadline: Dec. 2026 |
2.089 |
| 2.089 | 550 | 2026 | Factory | PRODUCTION | 10. Cubic meters per ton of cement: 0.245 m³/t cement | 10.1 Monitoring of leak detection. 10.2 Modifying the fire protection system layout. |
I consume natural resources. | 0,245 | 0,000 | 0,0 | Head of Support Services / Head of Electrical Maintenance | December 31, 2026 | 10.1 Expected deadline: Dec. 2026 10.2 Expected deadline: Dec. 2026 |
2.089 |
| 2.089 | 551 | 2026 | Factory | PRODUCTION | 11. Number of R&D&I projects on CO2 capture: 2 | 11.1 CAPTUS Project 11.2 Corefuel 25 11.3 Horizon CL5 |
Climate change | 2,000 | 0,000 | 0,0 | Address | October 31, 2027 | 11.1 Target date: Oct. 2027 11.2 Target date: Dec. 2026. Goal by 2026: Processing 11.3 Target date: Dec. 2026. Goal by 2026: Processing |
2.089 |
| 2.089 | 552 | 2026 | Factory | PRODUCTION | 12. Digitization of environmental metrics | 12.1 Launch of the APLANET Sustainability Platform. 12.2 Ecomundis EMAS Platform. |
Environmental Information | 2,000 | 0,000 | 0,0 | Head of Environment/Corporate Sustainability Division | December 31, 2026 | 12.1 Expected deadline: Dec. 2026 12.2 Expected deadline: June 2026. |
2.089 |
| userid | wdt_ID | Year | Center | Life Cycle Phase | Impact/Associated Impact | post_author |
 |
Legal compliance analysis |
Legal and regulatory compliance
The organization has a procedure and system for the identification of legal requirements, as well as for periodic evaluation to ensure full compliance. The following is a list of current environmental permits and/or authorizations, as well as a summary of their validity.
The activities carried out by the Mataporquera factory are carried out in accordance with the applicable European, national, regional and local environmental regulations in force, as well as with the specific requirements of each facility and the mandatory environmental authorization or permit. The evaluation of the legal compliance is carried out periodically and procedurally requirement by applicable requirement.
Throughout 2025, periodic reviews of applicable environmental legislation at the European, national, regional, and local levels were conducted and incorporated into the list of applicable environmental regulations and legal requirements (DM-02/1) by the Environmental Coordinator and the Energy Coordinator, with reference to the SALEM bulletins.
European environmental legislation:
- REGULATION 2025/40 of December 19, 2024, on packaging and packaging waste, amending Regulation (EU) 2019/1020 and Directive (EU) 2019/904 and repealing Directive 94/62/EC (Text
- relevant for EEA purposes).
- REGULATION 2025/40 of December 19, 2024, on packaging and packaging waste, amending Regulation (EU) 2019/1020 and Directive (EU) 2019/904 and repealing Directive 94/62/EC (Text with EEA relevance).
Development of national energy regulations:
- ROYAL DECREE-LAW 7/2025, of June 24, approving urgent measures to strengthen the electricity system.
- ROYAL DECREE 214/2025, of March 18, establishing the registry for carbon footprints, offsets, and carbon dioxide absorption projects, and requiring the calculation of carbon footprints and the preparation and publication of greenhouse gas emission reduction plans.
List of permits, authorizations and declarations in force
The Integrated Environmental Authorization is an authorization granted by the Government of Cantabria, where the technical requirements and the control regime to be followed for most of the environmental aspects are included. We also have the Resolution of February 9, 2023 of Concession of water exploitation for industrial uses.
In 2025, the following authorizations were processed or resolved:
- In September, it was reported that a test was conducted to evaluate fuel blending at over 2,800 kcal/kg during September and October.
- In July, a request was submitted for a non-substantial amendment to the AAI to recover carbonate sludge prior to conducting an industrial trial involving 450 metric tons of this material. The tests will be conducted in October. A request was also made to include the option of bringing in declassified olive pomace as a product. Expansion of the LER catalog to include the following generated wastes: aerosols and metal containers. Correction of errors in the AAI: Hazardous waste minimization plan Hazardous continuous monitoring systems for the cooler and cement mill.
- On April 16, a test was conducted using Tycsa’s alternative fuel, lubricating soap, with negative results regarding dust emissions in the hopper discharge area and at the location of the metal detector at the transition from the hopper to the conveyor belt. It was decided to conduct a subsequent test using the pneumatic discharge and silo transport system.
- Authorization as a manager of Hazardous Hazardous waste Hazardous the Autonomous Community of Madrid. Legal requirement under Article 33.2 of Law 7/2022 on Waste and Contaminated Soil. Registration in accordance with the conditions of the Integrated Environmental Authorization. Received in February 2025.
Regulatory Compliance Summary
The most relevant legal references applicable to our activity are the following:
- Resolution of July 18, 2005 of the General Director of the Environment, which gives effect to the integrated environmental authorization granted to CEMENTOS ALFA, S.A. for the cement production activity, in the municipality of Valdeolea. Substantial Modification added in Resolution of November 23rd, 2023.
- Resolution of the Directorate General for the Environment of December 28, 2012 issuing Greenhouse Gas Emission Authorization in application of Commission Regulation (EU) 601, as last amended by Resolution of September 29, 2021.
- Approval of the Methodological Monitoring Plan dated July 27, 2021.
- Mayor's Decree of 1982 for the granting of an activity license for the transformation of the manufacturing process to a dry process.
- Resolution of May 8, 1996 for the concession of water use for industrial purposes.
- Resolution of June 13, 2011 for the revision of the authorization to discharge wastewater from an office building of a quarry in the town of Mataporquera in the municipality of Valdeolea (Cantabria).
- Resolution of March 15, 2019 to grant authorization for emissions into the atmosphere from the Quarry facility.
- Approval of the extension of the Exploitation of the ALFA quarry concession by Resolution of June 2020.
- Received in February 2021 Environmental Impact Statement for the project "Extension of the "Alfa-2 (1st fraction)" exploitation concession term, No. 16,241-01 (Cantabria and Palencia), February 2021.
- Resolution of August 2, 2021 of referral of characteristics and conditions of water use of the quarry pool.
- Resolution Authorizing the discharge of wastewater from the quarry pond in the town of Mataporquera in the municipality of Valdeolea (Cantabria), dated June 23, 2022.
There are several relevant new legislative developments that will arise in the year 2024 and will be incorporated into the requirements applicable to cement manufacturing.
- REGULATION (EU) 2024/590 of 7 February 2024 on substances that deplete the ozone layer, and repealing Regulation (EC) No. 1005/2009.
- REGULATION 2024/573 of the European Parliament and of the Council of 7 February 2024 on fluorinated greenhouse gases, amending Directive (EU) 2019/1937, and repealing Regulation (EU) No. 517/2014.
- REGULATION (EU) 2024/197 of 19 October 2023 amending Regulation (EC) No 1272/2008 with regard to the harmonized classification and labeling of certain substances.
- RESOLUTION of July 3, 2024, of the Directorate General for Energy Planning and Coordination, updating Annex I of Order TED/845/2023, of July 18, which approves the catalog of standardized energy efficiency measures.
|
Good environmental management practices |
Ecodesign and life cycle analysis
Life Cycle Assessment (LCA) of a product, process or technology is a methodology that attempts to identify, quantify and characterize the different potential environmental impacts associated with each stage of a product's life cycle. The LCA provides valuable information that allows the industry and users to make decisions aimed at improving the environmental performance of processes and products.
The cement sector, as a sector sensitive to sustainable development, has developed a life cycle analysis through AENOR's Global EPD Program, which has resulted in sectoral environmental product declarations (EPD).
Thus, the cement industry evaluates its impact, manages the use of different types of waste as raw materials or fuels, controls the destination of packaging, and monitors its process in search of the best environmental performance.
In order to promote transparency, the company has decided to draft and verify the Environmental Product Declarations for the cements it sells at all its plants in Spain. This work, carried out in 2025, culminated in the validation and publication of the six cements produced at the Mataporquera plant: CEM I 42.5 R, CEM I 52.5 R, CEM I 52.5 N (alkali-reduced), CEM II/A-L 42.5 N, CEM II/B-L 32.5 N, and CEM III/B 32.5 N-SR.
The GlobalEPD Declarations have been issued in accordance with the GlobalEPD-RCP-003 Cements Rules issued in accordance with the Rules contained in the UNE-EN 16908:2019+A1:2022 Standard. All environmental declarations are in accordance with European Standard EN 15804.
Reinforcing its commitment to the sustainability of its products, Cementos Portland Valderrivas has obtained the “sustainable” N mark (Ns mark) certification for all its cements. This mark is an evolution of AENOR’s traditional N quality mark and represents a new sustainability certification standard for industrial and construction products.
The Ns mark is the first certification in Spain that guarantees that a product is sustainable from an integral approach, evaluating technical and performance quality, environmental impact, social responsibility and corporate governance.
In the following link you can consult the corresponding Environmental Statement: AENOR - GlobalEPD Statements in force
Best practices in environmental management
Best Environmental Management Practices
The objectives for the 2026–2030 period have been updated based on the historical investment scenario, new legal requirements (currently under review and in the implementation phase), annual budget forecasts, internal CSRD information management projects, GCPV’s sustainability objectives, and carbon footprint management.
◉ Verification record
This Digital Environmental Statement has been verified by:
– AENOR CONFIA S.A.U.
The document with the highest validity—or, in the event of discrepancies—shall be the PDF digitally signed by the verifying body. This document is an accurate representation and printout of this Digital Environmental Declaration or rendered web page. Interested parties may download this rendered version here as a sample and as evidence of the immutability and consistency of the data validated in this DIGITAL ENVIRONMENTAL DECLARATION. DAD-EMAS-2025-MATAPORQUERA-29-05-26-L.pdf
Date of lastupdate: – Render version File No.: 0
ORGANIZATION: GRUPO CEMENTOS PORTLAND VALDERRIVAS - CENTER/s - COVERAGE: MATAPORQUERA FACTORY
ACCESS TO THE EUROPEAN REGISTRY: EUROPEAN COMMISSION
TRANSLATIONS OF THIS ENVIRONMENTAL STATEMENT: This EMAS Environmental Statement has been verified in its original language. The browsers used by stakeholders for consultation, or the Platform RightSupply itself, may automatically translate its direct transcription, without the certifying body considering its translated content as validated a priori. Methods such as sworn translation are recommended for this purpose.
EXTERNAL LINKS AND AUDIOVISUAL CONTENT: This EMAS Environmental Statement has been verified in its entirety, with the exception of external links and audiovisual or videographic content that may have been included for complementary purposes.
DIGITALIZATION: Digitization of environmental statements is a best practice with multiple sustainability benefits. By eliminating the use of paper, a significant reduction in energy and water consumption is achieved, which in turn minimizes the carbon footprint. This digital transition not only supports the environment, but also improves data accuracy and consistency, optimizing management efficiency, environmental reporting and access to information for stakeholders. This initiative was recognized as a best practice in 2022 within the European Union's INTERREG EUROPE public policy program (ENHANCE EMAS), underlining its importance in promoting a greener and more efficient administration across Europe.
CO₂ eq:stands forcarbon dioxide equivalent. It is used to measure the impact of different greenhouse gases on global warming by converting emissions of these gases into the equivalent amount of carbon dioxide (CO₂) that would produce the same effect.
EMAS: Eco-Management and AuditScheme. It is a voluntary environmental management system developed by the European Union for organizations that wish to assess, manage, and improve their environmental performance.
GJ:Unitof energy. A gigajoule is a unit of energy measurement, equivalent to one billion joules (J).
LPG: Liquefied PetroleumGas. It is a mixture of gaseous hydrocarbons, primarily propane and butane, which are liquefied to facilitate storage and transport.
GN: NaturalGas.
ISO: International Organization for Standardization. It is an entity that develops international standards for various products, services and management systems.
kt:Unitof mass equal to 1,000 tons.
MWh:Unitof energy in megawatt-hours
NACE: is a standard that allows the classification of the different economic activities carried out in the EU, facilitating the comparison of data between countries and the preparation of homogeneous statistics.
PPA:PowerPurchase Agreement. This is a long-term contract between an energy buyer and a renewable energy producer that sets forth the terms and conditions for the sale and purchase of electricity.
S1: Scope 1 for CO2eq emissions.
S2:Scope2 for CO2eq emissions.
S3:Scope3 for CO2eq emissions.
Units:Unit. Units concentration: Unit of concentration.
Units : Productionunit.
UNE:standsfor the Spanish Association for Standardization. It is the body responsible for developing technical standards in Spain, acting as the national standardization body. UNE promotes quality, safety, and efficiency in products and services through the development and dissemination of standards.
∑ (uppercase sigma):usedin mathematics to represent the sum of a series of terms.
Template: 2026 Final